

SIST EN 15594:2026
(Main)Railway applications - Infrastructure - Restoration of rails by electric arc welding
- Abstract
This document specifies restoration by electric arc welding and is limited to the head of the rails only.
This document describes the approval systems for consumables and procedures used in manual metal arc and flux cored metal deposit rail repair welding. This document includes the quality-related tasks and responsibilities of personnel involved in the electric arc repair welding of rails. This document applies to plain rail and switches and crossings manufactured from new Vignole railway rails R200, R220, R260, R260Mn, and R350HT grades rails of 27 kg/m and above as contained in EN 13674-1, EN 13674-2 and EN 13674-4.
The permitted welding processes are limited to Electric Arc (EA) in accordance with EN ISO 4063 and are by description Process No 111: SMAW (Shielded Metal Arc Welding) and Process No 114: FCAW (Flux Cored Arc Welding).
This document can be applied in situ, at line side or at out of track locations. The flash welded leg ends of austenitic manganese steel crossings are included in this document, except when located within 500 mm of manganese crossings. Where repairs are required within 500 mm, refer to EN 16725.
- Status
- Published
- Public Enquiry End Date
- 30-Apr-2025
- Publication Date
- 28-Oct-2026
- Technical Committee
- IŽNP - Reilway applications
- Current Stage
- 6060 - National Implementation/Publication (Adopted Project)
- Start Date
- 28-Oct-2026
- Due Date
- 02-Jan-2027
- Completion Date
- 29-Oct-2026
SIST EN 15594:2026 is a SIST standard for railway applications covering restoration of rails by electric arc welding. It specifies how rail-head repair welding is approved and controlled, including consumables, welding procedures, contractors, and personnel. In practice, it is the document for railway authorities, contractors, welders, and inspectors who need a common method for rail repair welding on plain rail and switches and crossings.
What does SIST EN 15594:2026 specify?
SIST EN 15594:2026 specifies restoration by electric arc welding, limited to the head of the rails. It sets out approval systems for consumables and procedures used in manual metal arc and flux cored metal deposit rail repair welding, and it assigns quality-related tasks and responsibilities for the people involved.
The standard applies to plain rail and switches and crossings made from new Vignole railway rails of the listed grades and rail weights, and it can be used in situ, at line side, or out of track locations. It also includes flash welded leg ends of austenitic manganese steel crossings, except when the repair is within 500 mm of manganese crossings, where EN 16725 applies.
| Annex | What it covers |
|---|---|
| Annex A | Supplementary information for track trials |
| Annex B | Example format for a Welding Procedure Specification (WPS) |
| Annex C | Specimen diploma for electric arc restoration welding of rails |
| Annex D | Specimen permit to restore rail by electric arc welding |
| Annex E | Track component names and their identification |
| Annex ZA | Relationship with EU Directive (EU) 2016/797 |
What are the key requirements of SIST EN 15594:2026?
SIST EN 15594:2026 is built around three control points: approval of the consumable and WPS, approval of the contractor, and qualification of the people doing the work. The practical message is that rail repair welding is treated as a controlled special process, not just a site activity.
Approval of consumables and WPS
Clause 4 requires consumable and WPS approval to follow EN ISO 15613, using a pre-production test model. The approving railway authority (RA) issues the approval certificate after successful track trials, and other railway authorities may ask for extra testing when local service or operating conditions need it.
Before testing, the standard requires technical information on the consumable, such as classification, chemical and batch analysis, storage, current and voltage range, polarity, dimensions, drying, marking, and the intended deposition technique. In practice, this means the manufacturer and contractor must define exactly what product is being approved and how it is to be used.
Clause 4 also requires batch testing and a defined set of laboratory and field checks, including mechanical tests, chemical analysis of undiluted weld metal, hardness, weld integrity, defect checks, porosity, crater behaviour, Open Circuit Voltage (OCV), and welding parameters. The consumable must also show acceptable general weldability through bead shape, cratering, spatter, slag behaviour, and strike and re-strike capability.
Laboratory tests and acceptance
Clause 4 requires laboratory tests on single bead, single layer, and multi-layer deposits on rail. These samples are inspected with magnetic particle testing (MT) or dye penetrant testing (PT), then sectioned for hardness and metallography as required.
The test geometry and preparation are defined so that the rail-head repair is assessed under controlled conditions similar to real work. The acceptance criteria cover hardness and metallurgical defects, with separate expectations for single-layer and multi-layer deposits. For the reader, this means the consumable must perform consistently on the rail steel grade and produce sound weld metal before it can be used in service.
Track trials
Clause 4.7 requires in-track trials in line with the RA requirements, using the approved WPS and the excavation details defined in the standard. The trials check surface cracking, flatness, rail head profile compliance, and weld integrity, with visual inspection, MT or PT, straightedge or electronic straightedge checks, and ultrasonic testing (UT) where required.
The trials must include both single-layer and multi-layer restorations, and inspection must continue over 12 months, with checks after 1 day, 1 month, 6 months, and 12 months as a minimum. Annex A adds that the test site must be documented in detail and kept free of visible and internal defects before welding.
Contractor approval and site control
Clause 5 requires the contractor to operate a quality management system in accordance with EN ISO 3834-2. It also requires approved inspection and testing, controlled subcontracting, suitable equipment, documented welding activities, proper storage and handling of consumables, protection of the infrastructure, RA-approved WPS use, approved pre-heating, supervision, traceability, audits, training, and documentation.
This is important in practice because the standard ties the welding result to the whole process chain. The contractor must be able to show which consumable, WPS, welder, location, and date were used for each weld.
Personnel qualification and permits
Clause 6 requires track welders to be qualified in accordance with EN ISO 9606-1 and trained in an RA-approved training establishment. The training includes consumable care, safety, rail grade identification, grinding, visual inspection, and geometric measurement.
After successful training, the welder receives a Diploma in Electric Arc Welding of Rails, shown in Annex C. To work in production, the welder also needs a Permit to restore rails by electric arc welding, with a maximum validity of 4 years, and Annex D gives the specimen format.
What terms does SIST EN 15594:2026 define?
SIST EN 15594:2026 uses a small set of core terms to separate approval, training, and production responsibilities.
- Railway authority (RA) - the railway regulator, infrastructure owner, or a custodian with delegated responsibility for the infrastructure.
- Contractor - a company approved by the RA to carry out rail restoration by electric arc welding on that infrastructure.
- Preliminary welding procedure specification (Pwps) - a tentative WPS used for approval welding before the procedure itself is approved.
- Welding procedure specification (WPS) - the approved procedure agreed by the RA for use on the railway infrastructure.
- Shielded Metal Arc Welding (SMAW) - manual electric arc welding using covered electrodes.
- Flux Cored Arc Welding (FCAW) - electric arc welding using flux cored wire.
- Training establishment - the approved organisation or centre that trains welders for this work.
Who uses SIST EN 15594:2026?
SIST EN 15594:2026 is used by railway authorities, infrastructure managers, welding contractors, consumable manufacturers, training centres, welders, and inspection staff. It supports approval of consumables and WPSs, qualification of welders, contractor auditing, and acceptance of repaired rails in track.
It is also relevant to buyers and engineers who specify repair welding for wheel burns, squats, headwear, sidewear, welding-zone defects, and other rail damage. The standard gives them a common basis for deciding what repairs are allowed, what evidence is needed, and how the repair is to be controlled.
What changed in SIST EN 15594:2026 from the previous edition?
SIST EN 15594:2026 supersedes EN 15594:2009. The foreword states these significant changes: updated normative references, additional rail steel grades, updated microstructure and macrostructure requirements, and the addition of Annex ZA.
Which standards are used with SIST EN 15594:2026?
SIST EN 15594:2026 relies on several companion standards for materials, testing, and procedure control.
- EN 13674-1 and EN 13674-4 - define the Vignole rail grades and sizes covered by the standard.
- EN 13674-2 - covers switch and crossing rails used with Vignole rails.
- EN 16725 - applies to restoration and repair of manganese crossings where this standard defers to it.
- EN ISO 4063 - gives welding process numbers, including the EA process descriptions used here.
- EN ISO 15607, EN ISO 15609-1, and EN ISO 15613 - define the general rules, WPS format, and pre-production qualification route for welding procedures.
- EN ISO 3834-2 - provides the comprehensive quality requirements for fusion welding.
- EN ISO 9606-1 - sets the welder qualification route for steel fusion welding.
- EN ISO 544 - covers delivery conditions and marking for welding consumables.
- EN ISO 17638, EN ISO 3452-1, EN ISO 6506-1, and EN ISO 6507-1 - support inspection, penetrant testing, and hardness testing.
- EN ISO 3580, EN ISO 14700, and EN ISO 18276 - support consumable classification.
What does the SIST EN 15594:2026 document contain?
SIST EN 15594:2026 contains approval flows for consumables and WPSs, laboratory test methods, track trial requirements, contractor approval rules, and personnel qualification and permit procedures. It also includes sample preparation details, inspection methods, acceptance criteria, and the information that must be recorded in trial reports and traceability records.
The annexes add practical templates and support material: a WPS example, a diploma specimen, a permit specimen, and track component names. Annex ZA links the standard to the essential requirements of EU Directive (EU) 2016/797 for railway interoperability.
Relations
- Replaces
SIST EN 15594:2009 - Railway applications - Track - Restoration of rails by electric arc welding - Effective Date
- 01-Dec-2026
- Effective Date
- 28-Jan-2026
Get Certified
Connect with accredited certification bodies for this standard
DVS-ZERT GmbH
German welding certification society.
CARES (UK Certification Authority for Reinforcing Steels)
UK certification for reinforcing steels and construction.
EWF/IIW (European/International Welding Federation)
International welding personnel certification.
Sponsored listings
Frequently Asked Questions
SIST EN 15594:2026 is a standard published by the Slovenian Institute for Standardization (SIST). Its full title is "Railway applications - Infrastructure - Restoration of rails by electric arc welding". This standard covers: This document specifies restoration by electric arc welding and is limited to the head of the rails only. This document describes the approval systems for consumables and procedures used in manual metal arc and flux cored metal deposit rail repair welding. This document includes the quality-related tasks and responsibilities of personnel involved in the electric arc repair welding of rails. This document applies to plain rail and switches and crossings manufactured from new Vignole railway rails R200, R220, R260, R260Mn, and R350HT grades rails of 27 kg/m and above as contained in EN 13674-1, EN 13674-2 and EN 13674-4. The permitted welding processes are limited to Electric Arc (EA) in accordance with EN ISO 4063 and are by description Process No 111: SMAW (Shielded Metal Arc Welding) and Process No 114: FCAW (Flux Cored Arc Welding). This document can be applied in situ, at line side or at out of track locations. The flash welded leg ends of austenitic manganese steel crossings are included in this document, except when located within 500 mm of manganese crossings. Where repairs are required within 500 mm, refer to EN 16725.
This document specifies restoration by electric arc welding and is limited to the head of the rails only. This document describes the approval systems for consumables and procedures used in manual metal arc and flux cored metal deposit rail repair welding. This document includes the quality-related tasks and responsibilities of personnel involved in the electric arc repair welding of rails. This document applies to plain rail and switches and crossings manufactured from new Vignole railway rails R200, R220, R260, R260Mn, and R350HT grades rails of 27 kg/m and above as contained in EN 13674-1, EN 13674-2 and EN 13674-4. The permitted welding processes are limited to Electric Arc (EA) in accordance with EN ISO 4063 and are by description Process No 111: SMAW (Shielded Metal Arc Welding) and Process No 114: FCAW (Flux Cored Arc Welding). This document can be applied in situ, at line side or at out of track locations. The flash welded leg ends of austenitic manganese steel crossings are included in this document, except when located within 500 mm of manganese crossings. Where repairs are required within 500 mm, refer to EN 16725.
SIST EN 15594:2026 is classified under the following ICS (International Classification for Standards) categories: 25.160.10 - Welding processes; 93.100 - Construction of railways. The ICS classification helps identify the subject area and facilitates finding related standards.
SIST EN 15594:2026 has the following relationships with other standards: It is inter standard links to SIST EN 15594:2009, SIST EN ISO/IEC 30111:2020. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
SIST EN 15594:2026 is associated with the following European legislation: EU Directives/Regulations: 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU, 2016/797/EU; Standardization Mandates: M/483, M/591. When a standard is cited in the Official Journal of the European Union, products manufactured in conformity with it benefit from a presumption of conformity with the essential requirements of the corresponding EU directive or regulation.
SIST EN 15594:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
01-december-2026
Nadomešča:
SIST EN 15594:2009
Železniške naprave - Infrastruktura - Obnova tirnic z električnim obločnim
varjenjem
Railway applications - Infrastructure - Restoration of rails by electric arc welding
Bahnanwendungen - Infrastruktur - Aufarbeitung von Schienen durch elektrisches
Lichtbogenschweißen
Applications ferroviaires - Infrastructure - Réparation des rails par soudage à l’arc
électrique
Ta slovenski standard je istoveten z: EN 15594:2026
ICS:
25.160.10 Varilni postopki in varjenje Welding processes
93.100 Gradnja železnic Construction of railways
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
EN 15594
EUROPEAN STANDARD
NORME EUROPÉENNE
October 2026
EUROPÄISCHE NORM
ICS 25.160.10 Supersedes EN 15594:2009
English Version
Railway applications - Infrastructure - Restoration of rails
by electric arc welding
Applications ferroviaires - Infrastructure - Réparation Bahnanwendungen - Infrastruktur - Aufarbeitung von
des rails par soudage à l'arc électrique Schienen durch elektrisches Lichtbogenschweißen
This European Standard was approved by CEN on 3 August 2026.
CEN members are bound to comply with the CEN/CENELEC Internal Regulations which stipulate the conditions for giving this
European Standard the status of a national standard without any alteration. Up-to-date lists and bibliographical references
concerning such national standards may be obtained on application to the CEN-CENELEC Management Centre or to any CEN
member.
This European Standard exists in three official versions (English, French, German). A version in any other language made by
translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC Management
Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2026 CEN All rights of exploitation in any form and by any means reserved Ref. No. EN 15594:2026 E
worldwide for CEN national Members.
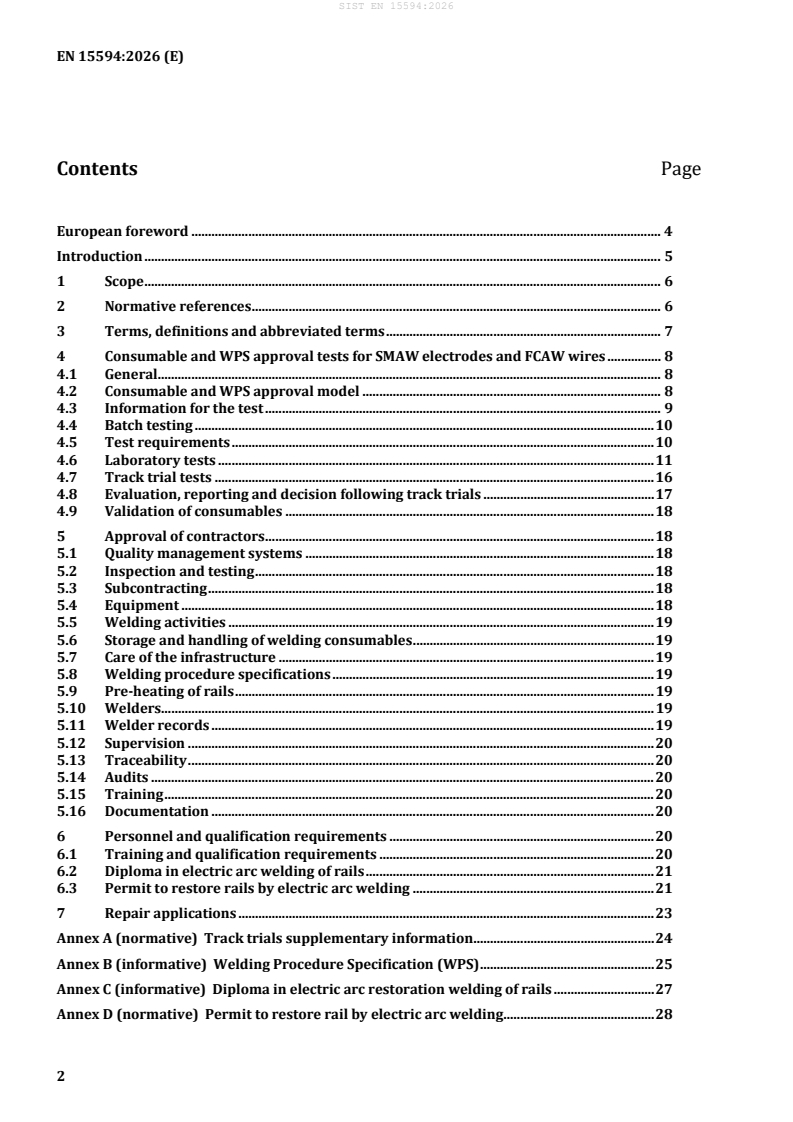
Contents Page
European foreword . 4
Introduction . 5
1 Scope . 6
2 Normative references . 6
3 Terms, definitions and abbreviated terms . 7
4 Consumable and WPS approval tests for SMAW electrodes and FCAW wires . 8
4.1 General. 8
4.2 Consumable and WPS approval model . 8
4.3 Information for the test . 9
4.4 Batch testing . 10
4.5 Test requirements . 10
4.6 Laboratory tests . 11
4.7 Track trial tests . 16
4.8 Evaluation, reporting and decision following track trials . 17
4.9 Validation of consumables . 18
5 Approval of contractors . 18
5.1 Quality management systems . 18
5.2 Inspection and testing . 18
5.3 Subcontracting . 18
5.4 Equipment . 18
5.5 Welding activities . 19
5.6 Storage and handling of welding consumables . 19
5.7 Care of the infrastructure . 19
5.8 Welding procedure specifications . 19
5.9 Pre-heating of rails . 19
5.10 Welders. 19
5.11 Welder records . 19
5.12 Supervision . 20
5.13 Traceability . 20
5.14 Audits . 20
5.15 Training . 20
5.16 Documentation . 20
6 Personnel and qualification requirements . 20
6.1 Training and qualification requirements . 20
6.2 Diploma in electric arc welding of rails . 21
6.3 Permit to restore rails by electric arc welding . 21
7 Repair applications . 23
Annex A (normative) Track trials supplementary information . 24
Annex B (informative) Welding Procedure Specification (WPS) . 25
Annex C (informative) Diploma in electric arc restoration welding of rails . 27
Annex D (normative) Permit to restore rail by electric arc welding . 28
Annex E (informative) Track components. 29
Annex ZA (informative) Relationship between this European Standard and the essential
requirements of EU Directive (EU) 2016/797 aimed to be covered . 30
Bibliography . 31
European foreword
This document (EN 15594:2026) has been prepared by Technical Committee CEN/TC 256 “Railway
applications”, the secretariat of which is held by DIN.
This European Standard shall be given the status of a national standard, either by publication of an
identical text or by endorsement, at the latest by April 2027, and conflicting national standards shall be
withdrawn at the latest by April 2027.
Attention is drawn to the possibility that some of the elements of this document may be the subject of
patent rights. CEN shall not be held responsible for identifying any or all such patent rights.
This document supersedes EN 15594:2009.
This document includes the following significant technical changes with respect to EN 15594:2009:
— normative references have been updated;
— additional rail steel grades have been included;
— microstructure and macrostructure requirements have been updated;
— an Annex ZA has been included.
The purpose of this document is to unify the restoration of rail electric arc welding across Europe. The
document provides control systems for the approval and qualification of welding processes, welding
procedures, welding consumables, contractors and welders for the successful delivery of welds into track.
This document has been prepared under a standardization request addressed to CEN by the European
Commission. The Standing Committee of the EFTA States subsequently approves these requests for its
Member States.
For the relationship with EU Legislation, see informative Annex ZA, which is an integral part of this
document.
Any feedback and questions on this document should be directed to the users’ national standards body.
A complete listing of these bodies can be found on the CEN website.
According to the CEN-CENELEC Internal Regulations, the national standards organisations of the
following countries are bound to implement this European Standard: Austria, Belgium, Bulgaria, Croatia,
Cyprus, Czech Republic, Denmark, Estonia, Finland, France, Germany, Greece, Hungary, Iceland, Ireland,
Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Republic of North
Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and the United
Kingdom.
Introduction
Restoration of rails by electric arc welding is a special process requiring the coordination of welding and
grinding activities to establish confidence and reliability of the weld deposit and safety of the line.
Controls are to be in place from the design phase through to inspection. Incorrect selection of materials,
consumables or procedure can result in serious track welding failure.
It is important to strictly adhere to the correct application of the approved processes and the types of
repairs permitted to be carried out on various rail components. Only consumables approved by the
method described in this document should be used. The tasks and responsibilities of personnel involved
in restoration, e.g. planning, executing, supervising and inspection should be clearly defined.
1 Scope
This document specifies restoration by electric arc welding and is limited to the head of the rails only.
This document describes the approval systems for consumables and procedures used in manual metal
arc and flux cored metal deposit rail repair welding. This document includes the quality-related tasks and
responsibilities of personnel involved in the electric arc repair welding of rails. This document applies to
plain rail and switches and crossings manufactured from new Vignole railway rails R200, R220, R260,
R260Mn, and R350HT grades rails of 27 kg/m and above as contained in EN 13674-1, EN 13674-2 and
EN 13674-4.
The permitted welding processes are limited to Electric Arc (EA) in accordance with EN ISO 4063 and are
by description Process No 111: SMAW (Shielded Metal Arc Welding) and Process No 114: FCAW (Flux
Cored Arc Welding).
This document is applicable in situ, at line side or at out of track locations. The flash welded leg ends of
austenitic manganese steel crossings are included in this document, except when located within 500 mm
of manganese crossings. Where repairs are required within 500 mm, refer to EN 16725.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 13674-1:2011+A1:2017, Railway applications - Track - Rail - Part 1: Vignole railway rails 46 kg/m and
above
EN 13674-4:2019, Railway applications - Track - Rail - Part 4: Vignole railway rails from 27 kg/m to, but
excluding 46 kg/m
EN 17343:2023, Railway applications - General terms and definitions
EN ISO 544:2024, Welding consumables - Technical delivery conditions for filler materials and fluxes - Type
of product, dimensions, tolerances and markings (ISO 544:2024, Corrected version 2026-02)
EN ISO 3452-1:2021, Non-destructive testing - Penetrant testing - Part 1: General principles (ISO 3452-
1:2021)
EN ISO 3834-2:2021, Quality requirements for fusion welding of metallic materials - Part 2: Comprehensive
quality requirements (ISO 3834-2:2021)
EN ISO 6506-1:2014, Metallic materials - Brinell hardness test - Part 1: Test method (ISO 6506-1:2014)
EN ISO 6507-1:2023, Metallic materials - Vickers hardness test - Part 1: Test method (ISO 6507-1:2023)
EN ISO 9606-1:2017, Qualification testing of welders - Fusion welding - Part 1: Steels (ISO 9606-1:2012
including Cor 1:2012 and Cor 2:2013)
EN ISO 15607:2019, Specification and qualification of welding procedures for metallic materials - General
rules (ISO 15607:2019)
EN ISO 15609-1:2019, Specification and qualification of welding procedures for metallic materials -
Welding procedure specification - Part 1: Arc welding (ISO 15609-1:2019)
EN ISO 15613:2025, Specification and qualification of welding procedures for metallic materials -
Qualification based on a pre-production welding test (ISO 15613:2025)
3 Terms, definitions and abbreviated terms
For the purposes of this document, the terms and definitions given in EN 17343:2023 and the following
apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp
— IEC Electropedia: available at https://www.electropedia.org/
3.1
railway authority
RA
either the railway regulator or the owner of a railway infrastructure or the custodian with a delegated
responsibility for a railway infrastructure
3.2
contractor
company approved by a railway authority to carry out the restoration of rails by electric arc welding on
that infrastructure
3.3
FCAW
flux cored arc welding
3.4
SMAW
shielded metal arc welding
3.5
preliminary welding procedure specification
Pwps
tentative welding procedure specification, which is assumed to be adequate by the manufacturer, but
which has not been approved
Note 1 to entry: Welding of test pieces needed for approval of a welding procedure specification shall be carried
out based on a preliminary welding procedure specification.
3.6
weld procedure specification
WPS
procedure approved to European standards and agreed by the RA for use on the railway infrastructure
3.7
training establishment
welder training organisation or centre approved by the railway authority or alternatively a welder
training organisation or centre approved by and belonging to a railway authority
3.8
running surface
curved surface defined by the longitudinal displacement of a straight line perpendicular to the centre-
line of the track and tangential to both running tables
3.9
PT
dye penetrant inspection
4 Consumable and WPS approval tests for SMAW electrodes and FCAW wires
4.1 General
The approval of consumables and the related WPS shall follow the requirements of EN ISO 15613:2025.
Welding fume shall be removed from the welding environment by the means of local exhaust ventilation,
where this is not possible approved respiratory protective equipment shall be used.
4.2 Consumable and WPS approval model
The following flow chart Figure 1 describes how a consumable and its related WPS shall be approved.
WPS approval shall follow the principle of EN ISO 15613:2025 approval by a pre-production test.
Figure 1 — Approval process for a consumable and its related WPS
NOTE These track trials are undertaken by the approving RA.
The approving RA shall issue an approval certificate upon successful outcome of track trial.
Other railway authorities may require further tests to verify suitability for special service/operational
conditions or deposition techniques.
4.3 Information for the test
The standards quoted below are given for information only:
— toxicity threshold levels;
— SMAW electrode classification in accordance with EN ISO 3580:2017;
— wire electrodes classification in accordance with EN 14700:2022;
— tubular covered electrodes in accordance with EN ISO 18276:2024;
— chemical analysis and batch analysis;
— storage requirements with manufacturers recommendations;
— current range/voltage range/polarity;
— availability of vacuum sealed SMAW electrodes;
— dimensions, length and diameter;
— FCAW spool size/weight availability;
— drying requirements;
— description of marking system;
— optimum deposition technique.
4.4 Batch testing
The batch testing criteria are:
— concentricity and dimensions;
— chemical composition;
— consumable performance, e.g. wire behaviour.
4.5 Test requirements
4.5.1 List of tests
— mechanical tests;
— chemical analysis of undiluted weld metal with batch verification;
— hardness;
— weld integrity (laboratory conditions);
— crack free;
— defect level;
— porosity;
— craters;
— Open Circuit Voltage (OCV) requirements;
— welding parameters.
4.5.2 Information to be confirmed
Marking and branding shall be carried out before and after drying.
4.5.3 Statement on the general weldability
The statement on the general weldability shall include the following information:
— bead shape;
— cratering;
— spatter;
— slag characteristics;
— strike and re-strike capability;
— other relevant information.
These checks are carried out on one bead, one layer and five layers.
The one bead test checks for cracking after grinding.
The single layer test checks the behaviour of weld deposit on rail steel.
The five-layer test checks the behaviour of weld metal on weld metal.
In single and five-layer deposits macro, micro and hardness HV tests are employed.
The five-layer test is finish ground and ultrasonic testing applied.
4.6 Laboratory tests
4.6.1 Purpose
The purpose of the laboratory tests is to prove the suitability of the consumable to successfully repair
appropriate grades of rail steel.
4.6.2 General requirements for laboratory tests
The following deposits are required for laboratory tests:
— single bead on rail: one sample required;
— single layer on rail: one sample required;
— multi-layers on rail: one sample required.
Deposits shall be subjected to PT in accordance with EN ISO 3452-1:2021.
4.6.3 Description of the sample for laboratory test
Figures 2 and 3 describe the requirements of sample size, excavation details and preheat measurement
positions.
Pre-heat point A shall be 75 mm from the end of the excavation on the running surface.
Pre-heat point B shall be at the full railhead flange height.
Length of the sample C shall be 600 mm minimum.
Figure 2 — Position of preheat measurement and sample size
The transverse excavation for trials shall be 100 % of the railhead width.
Key
D depth of excavation
S slope (S ≥ 5D)
L length (L + 2S ≥ 200 mm)
The dimension D shall be such that the surface of the final layer is level with the surface of the parent rail
after grinding.
Figure 3 — Excavation dimensions
4.6.4 Single bead on rail tests
4.6.4.1 Purpose
This test is used to demonstrate the consumable’s compatibility with welding of rail steel before carrying
out further detailed tests. This deposition is without any excavation and provides information regarding
the bead shape, slag detachability, spatter, strike and re-strike capability.
4.6.4.2 Description
The sample shall be a minimum length of 600 mm in an appropriate grade of rail steel. The sample shall
be lightly ground on the running surface to give a clean oxide-free finish. The sample shall be preheated
in accordance with the Pwps and the position of pre-heat measurement in accordance with 4.6.3. For
SMAW only the deposit shall be made to maximum electrode recovery using the manufacturer’s
parameters.
4.6.4.3 Deposit examination and assessment
The deposit shall be cleaned removing all slag and spatter. Initially, the deposit shall be examined visually
in the as-welded condition.
Following visual examination, the bead shall be ground until 0,5 mm - 0,8 mm remains above the rail
surface. Following grinding the deposit shall be examined using visual and PT methods. The deposit shall
be assessed in accordance with 4.6.9.
If the weld deposit fails PT examination, the test shall be terminated. The approval of this consumable for
welding this grade shall be declined.
4.6.5 Single layer deposit on rail tests
4.6.5.1 Purpose
The purpose of this test is to establish the effects of dilution on a single layer and to check the integrity of
the weld deposit.
4.6.5.2 Description
The sample shall be a minimum length of 600 mm long in an appropriate grade of steel. The rail shall be
prepared in accordance with 4.6.3.
For SMAW only the length of the preparation shall be designed to use the full length of the electrode
minus 80 mm. This length can be derived from the single bead deposit on rail.
4.6.5.3 Deposit examination and assessment
The deposit shall be cleaned removing all slag and spatter and the surface checked using PT methods.
The deposit shall be sectioned, prepared and subjected to hardness testing and metallography in
accordance with 4.6.8. All results shall be assessed in accordance with 4.6.9.
If the weld deposit fails PT examination, the test shall be terminated.
4.6.6 Multi-layer deposit on rail tests
4.6.6.1 Purpose
The purpose of this test is to determine the integrity of the multi-layer weld metal on rail.
4.6.6.2 Description
The sample shall be a minimum length of 600 mm long in an appropriate grade of steel. The rail shall be
prepared in accordance with 4.6.3.
For SMAW the length of the preparation shall be designed to use the full length of the electrode minus
80 mm. This length can be derived from the single bead deposit on rail. On completion, the rail shall be
ground to rail head profile and shall contain a minimum of five layers and will facilitate a surface finish
suitable for Brinell hardness testing.
4.6.6.3 Deposit examination and assessment
The deposit shall be cleaned removing all slag and spatter and the surface checked using PT methods.
The deposit s
...