

SIST EN 2133:2026
(Main)Aerospace series - Cadmium plating of steels with specified tensile strength ≤ 1 450 MPa, copper, copper alloys and nickel alloys
- Abstract
This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed 235 °C.
- Status
- Published
- Public Enquiry End Date
- 17-Sep-2025
- Publication Date
- 20-Oct-2026
- Technical Committee
- I13 - Imaginarni 13
- Current Stage
- 6060 - National Implementation/Publication (Adopted Project)
- Start Date
- 19-Oct-2026
- Due Date
- 24-Dec-2026
- Completion Date
- 21-Oct-2026
SIST EN 2133:2026 is the Slovenian adoption of the European aerospace standard for electrolytic cadmium plating on steels, copper, copper alloys and nickel alloys. It specifies how the coating is prepared, heat treated, tested and accepted for parts and fasteners used in service up to 235 °C. The document is aimed at aerospace manufacturers, platers, fastener suppliers, inspectors and buyers who need a common basis for specifying and checking cadmium plating.
What does SIST EN 2133:2026 specify?
SIST EN 2133:2026 covers cadmium plating for parts and fasteners in steel with specified tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys. It organizes the requirements from the scope and definitions through process control, inspection, quality assurance and designation.
The document is structured into clauses 1 to 17, followed by two informative annexes.
| Annex | What it covers |
|---|---|
| Annex A | Process flow for the plating sequence |
| Annex B | Standard evolution form with the main changes from the previous edition |
What are the key requirements of SIST EN 2133:2026?
SIST EN 2133:2026 is built around process control and verification. The practical message is that the supplier must plan the plating route, document the part requirements from the purchaser, and prove performance by inspection and test.
Clause 5 defines the purpose of the process and the three plating types. Type 1 is as plated, Type 2 includes hexavalent chromium based post-treatment, and Type 3 excludes hexavalent chromium based post-treatment. If the purchase order does not name a type, the supplier chooses between Type 2 and Type 3. In practice, this affects the post-treatment route and the appearance and corrosion behavior expected from the finished part.
Clause 6 sets limits on where cadmium plated parts may be used. Contact with titanium, titanium alloys, fuels and fuel lines is restricted by service temperature. This matters for designers and buyers because the coating is not suitable everywhere in an aircraft assembly.
Clause 7 sets coating thickness classes A, B and C, unless a product standard or definition document gives different values. The note makes clear that the thickness applies to the cadmium coating, including post-treatment, while the nickel strike is treated as negligible. In practice, the part drawing or purchase order must identify the thickness class or another agreed requirement.
Clause 8 lists the information the purchaser must give the manufacturer. This includes the designation, substrate standard, metallurgical condition, areas to be treated, measuring points, heat treatment times and temperatures, contact points, finishing operations and the test basis. This is the information the shop needs to avoid masking errors, wrong heat treatment and unclear inspection points.
Clauses 9 to 12 control the preparation and sequence of work. Welding, soldering, brazing, mechanical work and heat treatments must be completed first. The standard also covers stress relief for steel parts, masking of areas that must stay uncoated, surface pre-treatment, optional nickel strike, cadmium plating, hydrogen-embrittlement-relief heat treatment, post-treatment and removal of defective coating. In practice, these clauses prevent damage to the base material and keep the plating process repeatable.
Clause 10.5 and Clause 11 are especially important when additives or post-treatment are used. Brighteners may be used only with verification that they do not introduce hydrogen embrittlement, and wetting agents are allowed if they do not worsen embrittlement behavior. Hydrogen-embrittlement-relief heat treatment is tied to a defined time window after plating, and Type 2 and Type 3 have different post-treatment routes. This is critical for high-strength steel parts and for flight-safety fasteners.
Clause 13 sets the required characteristics of the finished coating. The surface must be uniform and free from defects such as burning, pits, exfoliation and blisters. The clause also covers adhesion, hydrogen embrittlement and corrosion resistance, with different expectations for parts and fasteners and for the different plating types. For users, this is the acceptance target for the finished item.
Clause 14 and Clause 15 define the test methods and the periodic tests. Process approval and part acceptance use visual inspection, adhesion tests, thickness measurements, hydrogen-embrittlement tests and corrosion tests. Clause 15 groups the recurring checks on samples so that the supplier keeps proving that the process remains stable over time.
Clause 16 links the process to aerospace quality assurance. The manufacturer must be an approved production organization and maintain a quality management system such as EN 9100 or an equivalent accepted system. The clause also covers process approval, acceptance, reprocessing and periodic chemical analysis of the baths. This is what keeps the plating line under controlled production discipline.
What terms does SIST EN 2133:2026 define?
- batch - Parts of the same type treated at the same time in the same baths; for mechanical parts, this also ties to hydrogen-embrittlement relief carried out together.
- pre-production part - A part representative of future production, used to prove the process before full series production.
- brighteners - Organic or metallic additives used in alkaline cyanide cadmium baths to influence crystal formation and the final deposit.
- wetting agents - Chemicals added to lower surface tension so the bath spreads and penetrates surfaces more effectively.
- UTS - Ultimate tensile strenght - The strength measure used to classify the steel substrate and set heat-treatment and embrittlement controls.
- Type 1 / Type 2 / Type 3 - The three cadmium plating options used for ordering and process control, distinguished by whether and how hexavalent chromium based post-treatment is applied.
Who uses SIST EN 2133:2026?
SIST EN 2133:2026 is used by aerospace part manufacturers, fastener suppliers, electroplating shops, quality managers, test laboratories and purchasing teams. They use it to specify the coating, choose the process sequence, agree inspection points, select test methods and decide whether a batch can be accepted. It is also relevant to design engineers who must check whether cadmium plated parts are suitable for the service environment and assembly materials.
What changed in SIST EN 2133:2026 from the previous edition?
SIST EN 2133:2026 supersedes EN 2133:2020. The European foreword and Annex B list these main changes:
- nickel strike is optional instead of mandatory;
- the definitions of brighteners and wetting agents are clarified;
- the heat treatment provisions are clarified;
- de-embrittlement heat treatment after removal and re-plating is allowed if both steps stay within the stated time window;
- post-treatment information is added for Type 3;
- an introductory sentence is added before the three plating types;
- Annex A is modified;
- EN 9100 is moved out of the normative references and into the bibliography.
Which standards are used with SIST EN 2133:2026?
The document relies on several companion standards for testing and sampling:
- Adhesion - EN 2828, EN ISO 2819 and EN ISO 2409 support burnishing, grid and cross-cut style adhesion checks.
- Thickness measurement - EN ISO 1463, EN ISO 2082, EN ISO 2177, EN ISO 2178 and EN ISO 3497 provide the measurement methods used for coating thickness.
- Hydrogen embrittlement - EN 2831, EN 2832, ASTM F519-18, NASM 1312-5 and NASM 1312-14 support the different tests for parts and fasteners.
- Corrosion resistance - EN ISO 9227 and ASTM B117-19 are the neutral salt spray methods used for performance verification.
- Sampling - ISO 2859-1 is used for attribute-based inspection sampling during acceptance.
- Companion references - EN 9100 appears in the bibliography as an example of an aerospace quality management system, and ISO 4520 is also listed in the bibliography.
What does the SIST EN 2133:2026 document contain?
SIST EN 2133:2026 contains the working sequence for cadmium plating, including masking, surface pre-treatment, optional nickel strike, plating, post-treatment and removal of defective coating. It also includes tables for heat treatment and hydrogen-embrittlement relief, a table of periodic test requirements, and a figure showing the process flow.
For inspection and qualification work, the document gives the methods to use for appearance, adhesion, thickness, hydrogen embrittlement and corrosion resistance. Annex A supports process planning, and Annex B records the technical evolution of the standard for users who need to track what changed between editions.
Relations
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Refers
SIST EN ISO 9227:2023 - Corrosion tests in artificial atmospheres - Salt spray tests (ISO 9227:2022) - Effective Date
- 21-Oct-2026
- Refers
SIST EN 2831:2001 - Aerospace series - Hydrogen embrittlement of steels - Test by slow bending - Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Refers
SIST EN 2832:2001 - Aerospace series - Hydrogen embrittlement of steels - Notched specimen test - Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 14-Oct-2026
- Effective Date
- 14-Oct-2026
- Effective Date
- 14-Oct-2026
Get Certified
Connect with accredited certification bodies for this standard

BUREAU VERITAS Certification Germany
Bureau Veritas certification in Germany.
Element Materials Technology
Materials testing and product certification.

AQMS Ltd.
AQMS provides ISO certification to SMEs across the UK.
Sponsored listings
Frequently Asked Questions
SIST EN 2133:2026 is a standard published by the Slovenian Institute for Standardization (SIST). Its full title is "Aerospace series - Cadmium plating of steels with specified tensile strength ≤ 1 450 MPa, copper, copper alloys and nickel alloys". This standard covers: This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed 235 °C.
This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed 235 °C.
SIST EN 2133:2026 is classified under the following ICS (International Classification for Standards) categories: 49.040 - Coatings and related processes used in aerospace industry. The ICS classification helps identify the subject area and facilitates finding related standards.
SIST EN 2133:2026 has the following relationships with other standards: It is inter standard links to SIST EN ISO 2082:2017, SIST EN ISO 1463:2021, SIST EN ISO 2819:2018, SIST EN ISO 2178:2016, SIST EN ISO 3497:2002, SIST EN ISO 9227:2023, SIST EN 2831:2001, SIST EN 2828:2001, SIST EN ISO 2177:2004, SIST EN 2832:2001, SIST EN ISO 2409:2020, SIST EN 6046:2026, SIST EN 4850:2022, SIST EN 4854-2:2020, SIST EN 6056:2019. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
SIST EN 2133:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
01-december-2026
Aeronavtika - Kadmiranje jekla z določeno natezno trdnostjo ≤ 1450 MPa z bakrom,
bakrovimi in nikljevimi zlitinami
Aerospace series - Cadmium plating of steels with specified tensile strength ≤ 1 450
MPa, copper, copper alloys and nickel alloys
Luft- und Raumfahrt - Cadmieren von Stählen mit einer Zugfestigkeit ≤ 1 450 MPa,
Kupfer, Kupferlegierungen und Nickellegierungen
Série aérospatiale - Cadmiage électrolytique des aciers de résistance ≤ 1 450 MPa, du
cuivre, des alliages de cuivre et des alliages de nickel
Ta slovenski standard je istoveten z: EN 2133:2026
ICS:
49.040 Prevleke in z njimi povezani Coatings and related
postopki, ki se uporabljajo v processes used in aerospace
letalski in vesoljski industriji industry
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
EN 2133
EUROPEAN STANDARD
NORME EUROPÉENNE
October 2026
EUROPÄISCHE NORM
ICS 49.040 Supersedes EN 2133:2020
English Version
Aerospace series - Cadmium plating of steels with
specified tensile strength 1 450 MPa, copper, copper
alloys and nickel alloys
Série aérospatiale - Cadmiage électrolytique des aciers Luft- und Raumfahrt - Cadmieren von Stählen mit einer
de résistance 1 450 MPa, du cuivre, des alliages de Zugfestigkeit 1 450 MPa, Kupfer, Kupferlegierungen
cuivre et des alliages de nickel und Nickellegierungen
This European Standard was approved by CEN on 17 August 2026.
CEN members are bound to comply with the CEN/CENELEC Internal Regulations which stipulate the conditions for giving this
European Standard the status of a national standard without any alteration. Up-to-date lists and bibliographical references
concerning such national standards may be obtained on application to the CEN-CENELEC Management Centre or to any CEN
member.
This European Standard exists in three official versions (English, French, German). A version in any other language made by
translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC Management
Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2026 CEN All rights of exploitation in any form and by any means reserved Ref. No. EN 2133:2026 E
worldwide for CEN national Members.
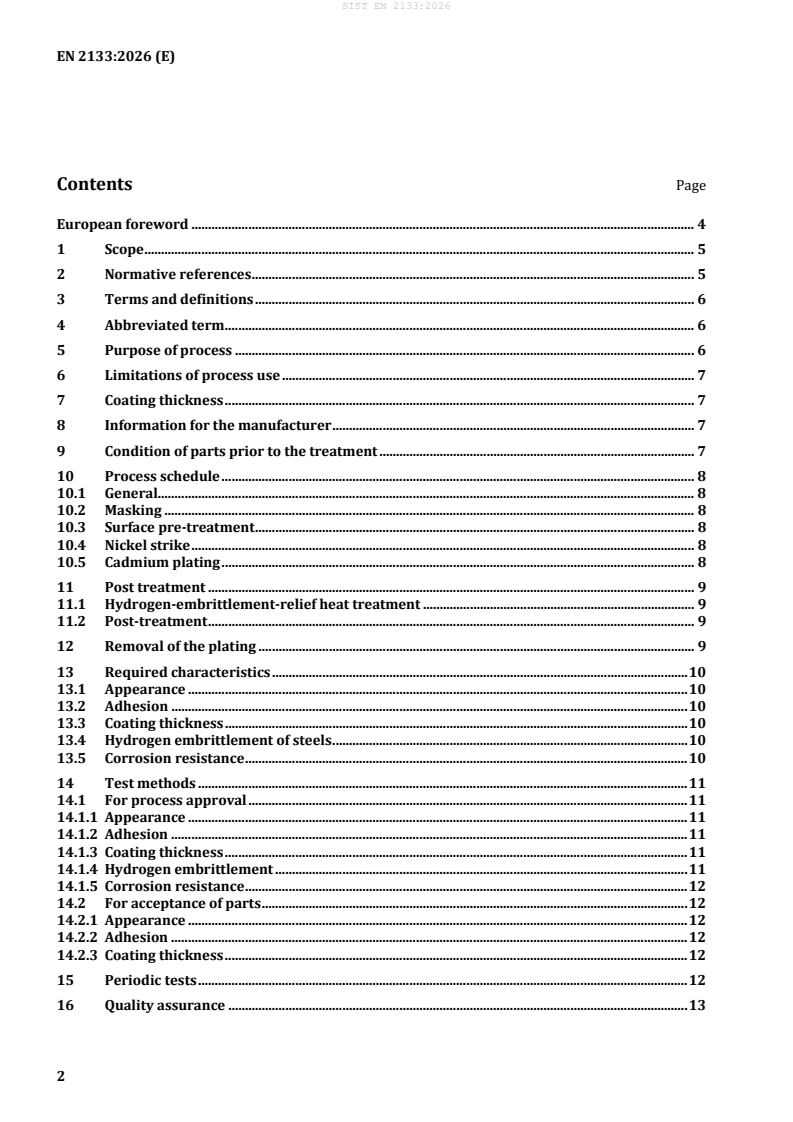
Contents Page
European foreword . 4
1 Scope . 5
2 Normative references . 5
3 Terms and definitions . 6
4 Abbreviated term . 6
5 Purpose of process . 6
6 Limitations of process use . 7
7 Coating thickness . 7
8 Information for the manufacturer . 7
9 Condition of parts prior to the treatment . 7
10 Process schedule . 8
10.1 General. 8
10.2 Masking . 8
10.3 Surface pre-treatment . 8
10.4 Nickel strike . 8
10.5 Cadmium plating . 8
11 Post treatment . 9
11.1 Hydrogen-embrittlement-relief heat treatment . 9
11.2 Post-treatment . 9
12 Removal of the plating . 9
13 Required characteristics . 10
13.1 Appearance . 10
13.2 Adhesion . 10
13.3 Coating thickness . 10
13.4 Hydrogen embrittlement of steels . 10
13.5 Corrosion resistance . 10
14 Test methods . 11
14.1 For process approval . 11
14.1.1 Appearance . 11
14.1.2 Adhesion . 11
14.1.3 Coating thickness . 11
14.1.4 Hydrogen embrittlement . 11
14.1.5 Corrosion resistance . 12
14.2 For acceptance of parts . 12
14.2.1 Appearance . 12
14.2.2 Adhesion . 12
14.2.3 Coating thickness . 12
15 Periodic tests . 12
16 Quality assurance . 13
16.1 Approval of the manufacturer . 13
16.2 Process approval. 13
16.3 Acceptance . 13
16.4 Reprocessing . 14
16.5 Periodic chemical analysis . 14
17 Designation . 14
Annex A (normative) Process flow . 15
Annex B (informative) Standard evolution form . 16
Bibliography . 19
European foreword
This document (EN 2133:2026) has been prepared by ASD-STAN.
After enquiries and votes carried out in accordance with the rules of this Association, this document has
received the approval of the National Associations and the Official Services of the member countries of
ASD-STAN, prior to its presentation to CEN.
This document shall be given the status of a national standard, either by publication of an identical text
or by endorsement, at the latest by April 2027, and conflicting national standards shall be withdrawn at
the latest by April 2027.
Attention is drawn to the possibility that some of the elements of this document may be the subject of
patent rights. CEN shall not be held responsible for identifying any or all such patent rights.
This document supersedes EN 2133:2020.
— making the nickel strike optional instead of mandatory;
— clarifying the definitions of brightener and wetting agent;
— providing clarification on the heat treatment;
— adding the option to perform de-embrittlement heat treatment after removal and re-plating if both
processes take less than 4 h;
— including information on post-treatment in type 3;
— adding an introductory sentence before the different types of cadmium plating;
— modifying Annex A.
See also Annex B for a list of technical changes.
According to the CEN-CENELEC Internal Regulations, the national standards organizations of the
following countries are bound to implement this document: Austria, Belgium, Bulgaria, Croatia, Cyprus,
Czech Republic, Denmark, Estonia, Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy,
Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Republic of North
Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and the
United Kingdom.
1 Scope
This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile
strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does
not exceed 235 °C.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 2828, Aerospace series — Adhesion test for metallic coatings by burnishing
EN 2831, Aerospace series — Hydrogen embrittlement of steels — Test by slow bending
EN 2832, Aerospace series — Hydrogen embrittlement of steels — Notched specimen test
EN ISO 1463, Metallic and oxide coatings — Measurement of coating thickness — Microscopical method
(ISO 1463)
EN ISO 2082, Metallic and other inorganic coatings — Electroplated coatings of cadmium with
supplementary treatments on iron or steel (ISO 2082)
EN ISO 2177, Metallic coatings — Measurement of coating thickness — Coulometric method by anodic
dissolution (ISO 2177)
EN ISO 2178, Non-magnetic coatings on magnetic substrates — Measurement of coating thickness —
Magnetic method (ISO 2178)
EN ISO 2409, Paints and varnishes — Cross-cut test (ISO 2409)
EN ISO 2819, Metallic coatings on metallic substrates — Electrodeposited and chemically deposited
coatings — Review of methods available for testing adhesion (ISO 2819)
EN ISO 3497, Metallic coatings — Measurement of coating thickness — X-ray spectrometric methods (ISO 3497)
EN ISO 9227, Corrosion tests in artificial atmospheres — Salt spray tests (ISO 9227)
ISO 2859-1, Sampling procedures for inspection by attributes — Part 1: Sampling schemes indexed by
acceptance quality limit (AQL) for lot-by-lot inspection
ASTM B117-19, Standard Practice for Operating Salt Spray (Fog) Apparatus
ASTM F519-18, Standard Test Method for Mechanical Hydrogen Embrittlement — Evaluation of
Plating/Coating Process and Service Environments
NASM 1312-5, Fastener test methods — Method 5 — Stress durability
NASM 1312-14, Fastener test methods — Method 14 — Stress durability, internally threaded fasteners
Published by: American Society for Testing and Materials (ASTM International), available at:
https://www.astm.org/.
Published by Aerospace Industries Association (AIA), available at: https://www.aia-aerospace.org/.
3 Terms and definitions
For the purposes of this document, the following terms and definitions apply.
ISO and IEC maintain terminological databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp
— IEC Electropedia: available at https://www.electropedia.org/
3.1
batch
unless otherwise specified, parts of the same type (shape, size, material), treated at the same time in the
same baths
Note 1 to entry: For mechanical parts, hydrogen embrittlement relieved at the same time.
3.2
pre-production part
part representative of future production
3.3
brightener
organic or metallic compound that, when added to alkaline cyanide cadmium plating baths, influence
the formation of the electrodeposited cadmium crystals
3.4
wetting agent
chemical that can be added to a liquid to reduce its surface tension and make it more effective in
spreading over and penetrating surfaces
4 Abbreviated term
For the purposes of this document, the following abbreviation applies:
UTS Ultimate tensile strength
5 Purpose of process
To ensure protection against corrosion or to reduce the effects of galvanic coupling when assembling
different materials, e.g. steel, aluminium or magnesium. Cadmium plating shall be of the following types
as specified in the purchase order:
— Type 1: as plated;
— Type 2: with hexavalent chromium based post-treatment;
— Type 3: without hexavalent chromium based post-treatment.
If the type is not specified by the purchase order, the choice between Type 2 or 3 is left to the supplier.
6 Limitations of process use
Contact of cadmium plated parts with titanium, titanium alloys, fuels and fuel lines is not recommended.
— It could be accepted at temperatures <150 °C.
— It is inadmissible at temperatures ≥150 °C.
7 Coating thickness
Unless otherwise specified in the product standard or definition document, the coating thicknesses are
as follows:
— Class A: 10 µm to 20 µm;
— Class B: 5 µm to 14 µm;
— Class C: 5 µm to 10 µm.
NOTE These thicknesses refer to the cadmium coating only (including the post-treatment). The nickel strike
thicknesses are consi
...