

EN 2133:2026
(Main)Aerospace series - Cadmium plating of steels with specified tensile strength ≤ 1 450 MPa, copper, copper alloys and nickel alloys
- Abstract
This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed 235 °C.
- Status
- Not Published
- Publication Date
- 06-Oct-2026
- Technical Committee
- ASD-STAN - Aerospace
- Drafting Committee
- ASD-STAN/D 4/S 6 - Surface treatments for Metallic
- Current Stage
- 6055 - CEN Ratification completed (DOR) - Publishing
- Start Date
- 17-Aug-2026
- Completion Date
- 17-Aug-2026
EN 2133:2026 is a CEN aerospace standard for electrolytic cadmium plating of steel parts and fasteners, copper, copper alloys and nickel alloys. It specifies the coating process, post-treatment, inspection and acceptance rules for parts whose service temperature does not exceed 235 °C.
The document is written for aerospace manufacturers, purchasers and inspectors who need to define the plating type, thickness class and test regime. In practice, it is the reference for getting corrosion protection and controlled galvanic behavior without leaving process choices unclear.
What does EN 2133:2026 specify?
EN 2133:2026 specifies the cadmium plating process for aerospace parts and fasteners and the checks needed to approve and accept that process. It is organized into clauses on scope, references, terms, symbols, purpose, process limits, coating thickness, manufacturer information, pre-treatment, process schedule, post-treatment, stripping, required characteristics, test methods, periodic tests, quality assurance and designation, plus two informative annexes.
| Annex | What it covers |
|---|---|
| A | Process flow, including the sequence from masking through plating and treatment |
| B | Standard evolution form and the main technical changes from the previous edition |
What are the key requirements of EN 2133:2026?
EN 2133:2026 sets out how to prepare, plate, treat, test and designate cadmium-coated aerospace parts so the coating performs as intended. The most important points are the process type, the limitations on use, the heat-treatment steps, the required surface condition and the test regime.
Process purpose, types and limits
EN 2133:2026 says cadmium plating is used to protect against corrosion and to reduce galvanic coupling when different materials are assembled. The document defines three types: Type 1 as plated, Type 2 with hexavalent chromium based post-treatment, and Type 3 without hexavalent chromium based post-treatment.
If the purchase order does not state Type 2 or Type 3, the supplier chooses between them. For the buyer, that means the order should state the finish expected on the delivered parts.
The document also limits contact with titanium, titanium alloys, fuels and fuel lines. That matters in assembly planning, because some material pairings are allowed only below a stated temperature and are not allowed at higher temperature.
Before plating: part condition and surface preparation
Clause 9 requires welding, soldering or brazing, mechanical operations and heat treatment to be completed before cadmium plating. It also calls for stress relief on steel parts according to the substrate condition, and shot peening, if specified, to be done after stress relief.
Clause 10 requires masking of areas that must not be plated, based on the purchaser’s information. Surface pre-treatment must remove contamination completely, and methods that can load the material with hydrogen should be avoided. In practice, this is the stage that prevents adhesion failures and later embrittlement problems.
Plating, brighteners and nickel strike
Clause 10 also covers nickel strike and the cadmium plating bath. Nickel strike may be used to improve adhesion, and on corrosion resisting steel it is optional if adhesion still meets the document’s requirements.
Cadmium plating should preferably be done without brighteners. If brighteners are used, the absence of hydrogen embrittlement has to be verified with the method named in the document. Wetting agents are permitted, but they must not worsen embrittlement behavior. For a buyer, this means bath chemistry is not just a production detail - it is part of the approval status of the process.
Post-treatment and stripping
Clause 11 requires hydrogen-embrittlement-relief heat treatment after plating, and the document ties that treatment to the substrate type. Type 1 has no post-treatment, Type 2 uses hexavalent chromium based post-treatment after the relief heat treatment, and Type 3 has no hexavalent chromium based post-treatment before or after the relief treatment.
Clause 12 allows both electrochemical and chemical stripping when plating has to be removed, but the stripping must not damage the base material or its dimensions. If stripping can introduce hydrogen, a relief treatment is required afterward unless replating and the follow-up heat treatment are completed within the time window defined by the standard.
Required characteristics and acceptance tests
Clause 13 defines the required appearance, adhesion, thickness, hydrogen-embrittlement performance and corrosion resistance. The coated surface must be uniform and free from obvious defects, and the type of post-treatment affects the acceptable color and finish.
For thickness, the document uses three coating thickness classes and makes clear that the cadmium thickness includes the post-treatment, while the nickel strike thickness is negligible. For acceptance, thickness is checked mainly where a 20 mm ball can reach the surface, which matters on complex shapes and recessed areas.
Hydrogen-embrittlement requirements are split between parts and fasteners. For fasteners, the document points to load-holding and crack-free performance under the named fastener test methods. For corrosion resistance, it uses neutral salt spray exposure with different acceptance limits depending on whether the part has chromate-based or chromate-free post-treatment.
Process approval, acceptance and periodic control
Clause 14 gives the test methods for process approval and for acceptance of parts. It covers visual inspection, burnishing and grid or tape adhesion tests, thickness measurement methods, hydrogen-embrittlement testing and salt spray testing. For thickness disputes, EN ISO 1463 is the reference method.
Clause 15 groups the periodic tests, and Clause 16 covers manufacturer approval, process approval, acceptance sampling, reprocessing and periodic chemical analysis of the baths. In practice, these clauses tell a supplier how to keep the process under control over time, not just for the first article.
What terms does EN 2133:2026 define?
EN 2133:2026 defines a small set of process terms that matter for production control and traceability.
- Batch - parts of the same type, shape, size and material treated at the same time in the same baths; for mechanical parts, this includes hydrogen-embrittlement relief at the same time.
- Pre-production part - a part that represents the future production item and is used for process checking before series release.
- Brighteners - organic or metallic additives used in alkaline cyanide cadmium baths to influence how the cadmium crystals form.
- Wetting agents - chemicals added to a liquid to reduce surface tension and improve spreading and penetration.
- UTS - ultimate tensile strength, the tensile strength symbol used to classify the steel substrate.
Who uses EN 2133:2026?
EN 2133:2026 is used by aerospace plating shops, fastener manufacturers, subcontract processors, quality departments and purchasers who specify cadmium coating on parts or fasteners. It is also used by test laboratories that carry out adhesion, coating thickness, hydrogen-embrittlement and corrosion tests.
For procurement teams, the standard helps define what type of cadmium finish is ordered and what evidence is required at acceptance. For production and QA teams, it sets the process steps, sampling approach and verification methods.
What changed in EN 2133:2026 from the previous edition?
EN 2133:2026 replaces EN 2133:2020 and carries the technical changes identified in the document.
- Nickel strike is optional instead of mandatory.
- The definitions of brighteners and wetting agents are clarified.
- The heat-treatment provisions are clarified.
- The standard adds the option to carry out de-embrittlement heat treatment after removal and replating if both processes take less than 4 h.
- Post-treatment information is added for Type 3.
- An introductory sentence is added before the different types of cadmium plating.
- Annex A is modified.
Which standards are used with EN 2133:2026?
EN 2133:2026 cites test and support standards for adhesion, thickness, hydrogen embrittlement, corrosion testing and sampling. The main references contribute as follows:
- EN 2828 - burnishing adhesion test for metallic coatings
- EN 2831 - slow bending test for hydrogen embrittlement of steels
- EN 2832 - notched specimen test for hydrogen embrittlement of steels
- EN ISO 1463 - microscopical thickness measurement, used as the reference method in disputes
- EN ISO 2082 - cadmium coatings with supplementary treatments on iron or steel
- EN ISO 2177 / EN ISO 2178 / EN ISO 3497 - coulometric, magnetic and X-ray thickness measurement methods
- EN ISO 2409 / EN ISO 2819 - grid test and review of adhesion methods
- EN ISO 9227 - neutral salt spray corrosion testing
- ISO 2859-1 - lot-by-lot acceptance sampling by attributes
- ASTM B117-19 - salt spray apparatus and test practice
- ASTM F519-18 - mechanical hydrogen-embrittlement evaluation
- NASM 1312-5 / NASM 1312-14 - stress durability tests for threaded fasteners
What does the EN 2133:2026 document contain?
EN 2133:2026 contains process guidance, inspection methods, acceptance criteria and control rules for cadmium plating in aerospace use. It includes tables for treatment conditions, coating thickness classes, hydrogen-embrittlement relief and periodic testing, plus a process flow in Annex A.
The body of the document also explains what information the manufacturer needs before work starts, how to handle masking and pre-treatment, how to remove and reapply the coating, and how to sample parts during acceptance. Annex B provides a compact record of the standard’s technical evolution.
Relations
- Effective Date
- 18-Dec-2024
Get Certified
Connect with accredited certification bodies for this standard

BUREAU VERITAS Certification Germany
Bureau Veritas certification in Germany.
Element Materials Technology
Materials testing and product certification.

AQMS Ltd.
AQMS provides ISO certification to SMEs across the UK.
Sponsored listings
Frequently Asked Questions
EN 2133:2026 is a draft published by the European Committee for Standardization (CEN). Its full title is "Aerospace series - Cadmium plating of steels with specified tensile strength ≤ 1 450 MPa, copper, copper alloys and nickel alloys". This standard covers: This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed 235 °C.
This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed 235 °C.
EN 2133:2026 is classified under the following ICS (International Classification for Standards) categories: 49.040 - Coatings and related processes used in aerospace industry. The ICS classification helps identify the subject area and facilitates finding related standards.
EN 2133:2026 has the following relationships with other standards: It is inter standard links to EN 2133:2020. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
EN 2133:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
oSIST prEN 2133:2025
01-september-2025
Aeronavtika - Kadmiranje jekla z določeno natezno trdnostjo ≤ 1 450 MPa z
bakrom, bakrovimi in nikljevimi zlitinami
Aerospace series - Cadmium plating of steels with specified tensile strength ≤ 1 450
MPa, copper, copper alloys and nickel alloys
Luft- und Raumfahrt - Cadmieren von Stählen mit einer Zugfestigkeit ≤ 1 450 MPa,
Kupfer, Kupferlegierungen und Nickellegierungen
Série aérospatiale - Cadmiage électrolytique des aciers de résistance ≤ 1 450 MPa, du
cuivre, des alliages de cuivre et des alliages de nickel
Ta slovenski standard je istoveten z: prEN 2133
ICS:
49.040 Prevleke in z njimi povezani Coatings and related
postopki, ki se uporabljajo v processes used in aerospace
letalski in vesoljski industriji industry
oSIST prEN 2133:2025 en,fr,de
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
oSIST prEN 2133:2025
oSIST prEN 2133:2025
DRAFT
EUROPEAN STANDARD
prEN 2133
NORME EUROPÉENNE
EUROPÄISCHE NORM
June 2025
ICS 49.040 Will supersede EN 2133:2020
English Version
Aerospace series - Cadmium plating of steels with
specified tensile strength 1 450 MPa, copper, copper
alloys and nickel alloys
Série aérospatiale - Cadmiage électrolytique des aciers Luft- und Raumfahrt - Kadmieren von Stählen mit einer
de résistance 1 450 MPa, du cuivre, des alliages de Zugfestigkeit 1 450 MPa, von Kupfer, von
cuivre et des alliages de nickel Kupferlegierung und von Nickellegierungen
This draft European Standard is submitted to CEN members for enquiry. It has been drawn up by the Technical Committee ASD-
STAN.
If this draft becomes a European Standard, CEN members are bound to comply with the CEN/CENELEC Internal Regulations
which stipulate the conditions for giving this European Standard the status of a national standard without any alteration.
This draft European Standard was established by CEN in three official versions (English, French, German). A version in any other
language made by translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC
Management Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
Recipients of this draft are invited to submit, with their comments, notification of any relevant patent rights of which they are
aware and to provide supporting documentation.
Warning : This document is not a European Standard. It is distributed for review and comments. It is subject to change without
notice and shall not be referred to as a European Standard.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2025 CEN All rights of exploitation in any form and by any means reserved Ref. No. prEN 2133:2025 E
worldwide for CEN national Members.
oSIST prEN 2133:2025
prEN 2133:2025 (E)
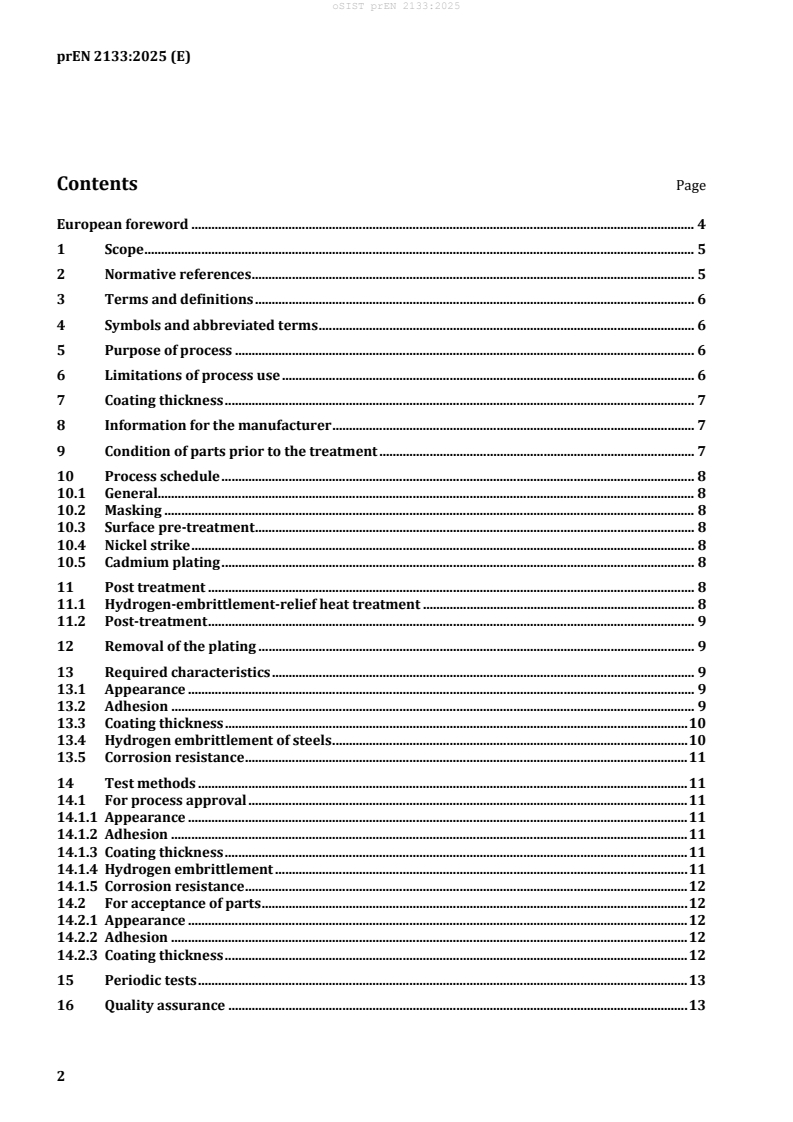
Contents Page
European foreword . 4
1 Scope . 5
2 Normative references . 5
3 Terms and definitions . 6
4 Symbols and abbreviated terms . 6
5 Purpose of process . 6
6 Limitations of process use . 6
7 Coating thickness . 7
8 Information for the manufacturer . 7
9 Condition of parts prior to the treatment . 7
10 Process schedule . 8
10.1 General. 8
10.2 Masking . 8
10.3 Surface pre-treatment . 8
10.4 Nickel strike . 8
10.5 Cadmium plating . 8
11 Post treatment . 8
11.1 Hydrogen-embrittlement-relief heat treatment . 8
11.2 Post-treatment . 9
12 Removal of the plating . 9
13 Required characteristics . 9
13.1 Appearance . 9
13.2 Adhesion . 9
13.3 Coating thickness . 10
13.4 Hydrogen embrittlement of steels . 10
13.5 Corrosion resistance . 11
14 Test methods . 11
14.1 For process approval . 11
14.1.1 Appearance . 11
14.1.2 Adhesion . 11
14.1.3 Coating thickness . 11
14.1.4 Hydrogen embrittlement . 11
14.1.5 Corrosion resistance . 12
14.2 For acceptance of parts . 12
14.2.1 Appearance . 12
14.2.2 Adhesion . 12
14.2.3 Coating thickness . 12
15 Periodic tests . 13
16 Quality assurance . 13
oSIST prEN 2133:2025
prEN 2133:2025 (E)
16.1 Approval of the manufacturer . 13
16.2 Process approval. 13
16.3 Acceptance . 13
16.4 Reprocessing . 14
16.5 Periodic chemical analysis . 14
17 Designation . 14
Annex A (informative) Process flow . 15
Annex B (informative) Standard evolution form . 16
Bibliography . 19
oSIST prEN 2133:2025
prEN 2133:2025 (E)
European foreword
This document (prEN 2133:2025) has been prepared by ASD-STAN.
After enquiries and votes carried out in accordance with the rules of this Association, this document has
received the approval of the National Associations and the Official Services of the member countries of
ASD-STAN, prior to its presentation to CEN.
This document is currently submitted to the CEN Enquiry.
This document will supersede EN 2133:2020.
prEN 2133:2025 includes the following significant technical changes with respect to EN 2133:2020:
— making the nickel strike optional instead of mandatory;
— clarifying the definitions of brighteners and wetting agents;
— providing clarification on the heat treatment;
— adding the option to perform de-embrittlement heat treatment after removal and re-plating if both
processes take less than 4 h;
— including information on post-treatment in type 3;
— adding an introductory sentence before the different types of cadmium plating;
— modifying Annex A.
See also Annex B for a list of technical changes.
oSIST prEN 2133:2025
prEN 2133:2025 (E)
1 Scope
This document specifies the electrolytic cadmium plating of parts and fasteners in steel of tensile strength
UTS ≤ 1 450 MPa, copper, copper alloys and nickel alloys, whose temperature in service does not exceed
235 °C.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 2828, Aerospace series - Adhesion test for metallic coatings by burnishing
EN 2831, Aerospace series - Hydrogen embrittlement of steels - Test by slow bending
EN 2832, Aerospace series - Hydrogen embrittlement of steels - Notched specimen test
EN ISO 1463, Metallic and oxide coatings - Measurement of coating thickness - Microscopical method (ISO
1463)
EN ISO 2082, Metallic and other inorganic coatings - Electroplated coatings of cadmium with
supplementary treatments on iron or steel (ISO 2082)
EN ISO 2177, Metallic coatings - Measurement of coating thickness - Coulometric method by anodic
dissolution (ISO 2177)
EN ISO 2178, Non-magnetic coatings on magnetic substrates - Measurement of coating thickness - Magnetic
method (ISO 2178)
EN ISO 2409, Paints and varnishes - Cross-cut test (ISO 2409)
EN ISO 2819, Metallic coatings on metallic substrates - Electrodeposited and chemically deposited coatings
- Review of methods available for testing adhesion (ISO 2819)
EN ISO 3497, Metallic coatings - Measurement of coating thickness - X-ray spectrometric methods (ISO
3497)
EN ISO 9227, Corrosion tests in artificial atmospheres - Salt spray tests (ISO 9227)
ISO 2859-1, Sampling procedures for inspection by attributes — Part 1: Sampling schemes indexed by
acceptance quality limit (AQL) for lot-by-lot inspection
ASTM B117-19, Standard Practice for Operating Salt Spray (Fog) Apparatus
ASTM F519-18, Standard test method for mechanical hydrogen embrittlement — Evaluation of
plating/coating process and service environment
NASM 1312-5, Fastener Test Methods — Method 5 — Stress Durability
NASM 1312-14, Fastener Test Methods — Method 14 — Stress Durability, Internally Threaded Fasteners
Published by: ASTM National (US) American Society for Testing and Materials, https://www.astm.org/.
Published by: AIA National (US) Aerospace Industries Association of America, https://www.aia-aerospace.org/.
oSIST prEN 2133:2025
prEN 2133:2025 (E)
3 Terms and definitions
For the purposes of this document, the following terms and definitions apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp
— IEC Electropedia: available at https://www.electropedia.org/
3.1
batch
unless otherwise specified, parts of the same type (shape, size, material), treated at the same time in the
same baths
Note 1 to entry: For mechanical parts, hydrogen embrittlement relieved at the same time.
3.2
pre-production part
part representative of future production
3.3
brighteners
organic or metallic compounds that, when added to alkaline cyanide cadmium plating baths, influence
the formation of the electrodeposited cadmium crystals
3.4
wetting agents
chemical that can be added to a liquid to reduce its surface tension and make it more effective in
spreading over and penetrating surfaces
4 Symbols and abbreviated terms
For the purposes of this document, the following symbols and abbreviations apply:
UTS Ultimate tensile strenght
5 Purpose of process
To ensure protection against corrosion or to reduce the effects of galvanic coupling when assembling
different materials, e.g. steel, aluminium or magnesium. Cadmium plating shall be of the following types
defined at the purchase order.
— Type 1: as plated;
— Type 2: with hexavalent chromium based post-treatment;
— Type 3: without hexavalent chromium based post-treatment.
If the type is not specified by the purchase order, the choice between Type 2 or 3 is left to the supplier.
6 Limitations of process use
Contact of cadmium plated parts with titanium, titanium alloys, fuels and fuel lines
— shall be avoided at temperatures < 150 °C;
oSIST prEN 2133:2025
prEN 2133:2025 (E)
— is inadmissible at temperatures ≥ 150 °C.
7 Coating thickness
Unless otherwise specified in the product standard or definition document, the coating thicknesses are
as follows:
— Class A: 10 µm to 20 µm;
— Class B: 5 µm to 14 µm;
— Class C: 5 µm to 10 µm.
NOTE These thicknesses refer to the cadmium coating only (including the post-treatment). The nickel strike
thicknesses are considered negligible.
8 Information for the manufacturer
— designation, see Clause 17;
— number of the substrate standard and metallurgical condition
...