


ASTM A681-08(2015)
(Specification)Standard Specification for Tool Steels Alloy
Standard Specification for Tool Steels Alloy
ABSTRACT
This specification covers the chemical, mechanical, and physical requirements for available wrought alloy tool steel products. The material shall be made by an electric melting process. It shall be made from ingots that have been reduced in cross section in such a manner and to such a degree as to ensure proper refinement of the ingot structure. Chemical composition, hardness, macrostructure and decarburization of the material shall conform to the requirements in accordance to the referenced ASTM documents itemized herein.
SCOPE
1.1 This specification covers the chemical, mechanical, and physical requirements for available wrought alloy tool steel products.
1.2 These products, which include hot or cold finished bar, plate, sheet, strip, rod, wire, or forgings, are normally fabricated into tools, dies, or fixtures. The selection of a material for a particular application will depend upon design, service conditions, and desired properties.
1.3 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are mathematical conversions to SI units that are provided for information only and are not considered standard.
General Information
Buy Standard
Standards Content (Sample)
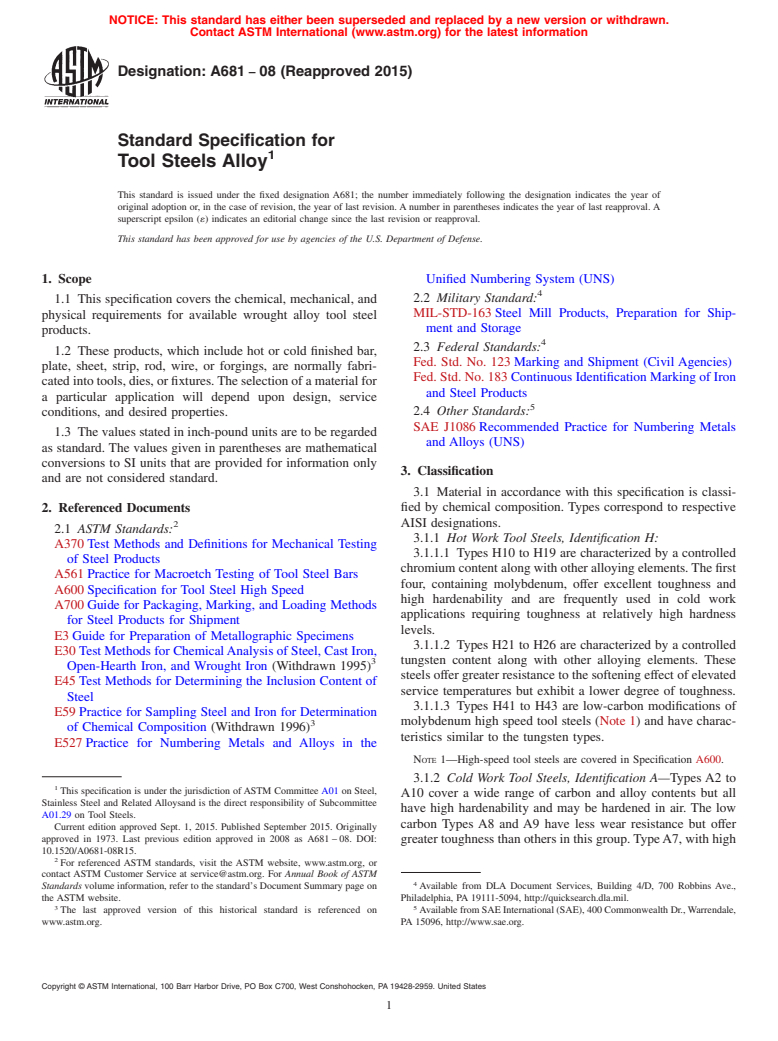
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation:A681 −08 (Reapproved 2015)
Standard Specification for
Tool Steels Alloy
This standard is issued under the fixed designation A681; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope Unified Numbering System (UNS)
2.2 Military Standard:
1.1 This specification covers the chemical, mechanical, and
MIL-STD-163 Steel Mill Products, Preparation for Ship-
physical requirements for available wrought alloy tool steel
ment and Storage
products.
2.3 Federal Standards:
1.2 These products, which include hot or cold finished bar,
Fed. Std. No. 123 Marking and Shipment (Civil Agencies)
plate, sheet, strip, rod, wire, or forgings, are normally fabri-
Fed. Std. No. 183 Continuous Identification Marking of Iron
cated into tools, dies, or fixtures.The selection of a material for
and Steel Products
a particular application will depend upon design, service
conditions, and desired properties. 2.4 Other Standards:
SAE J1086 Recommended Practice for Numbering Metals
1.3 The values stated in inch-pound units are to be regarded
and Alloys (UNS)
as standard. The values given in parentheses are mathematical
conversions to SI units that are provided for information only
3. Classification
and are not considered standard.
3.1 Material in accordance with this specification is classi-
fied by chemical composition. Types correspond to respective
2. Referenced Documents
2 AISI designations.
2.1 ASTM Standards:
3.1.1 Hot Work Tool Steels, Identification H:
A370 Test Methods and Definitions for Mechanical Testing
3.1.1.1 Types H10 to H19 are characterized by a controlled
of Steel Products
chromium content along with other alloying elements.The first
A561 Practice for Macroetch Testing of Tool Steel Bars
four, containing molybdenum, offer excellent toughness and
A600 Specification for Tool Steel High Speed
high hardenability and are frequently used in cold work
A700 Guide for Packaging, Marking, and Loading Methods
applications requiring toughness at relatively high hardness
for Steel Products for Shipment
levels.
E3 Guide for Preparation of Metallographic Specimens
3.1.1.2 Types H21 to H26 are characterized by a controlled
E30 Test Methods for ChemicalAnalysis of Steel, Cast Iron,
3 tungsten content along with other alloying elements. These
Open-Hearth Iron, and Wrought Iron (Withdrawn 1995)
steels offer greater resistance to the softening effect of elevated
E45 Test Methods for Determining the Inclusion Content of
service temperatures but exhibit a lower degree of toughness.
Steel
3.1.1.3 Types H41 to H43 are low-carbon modifications of
E59 Practice for Sampling Steel and Iron for Determination
3 molybdenum high speed tool steels (Note 1) and have charac-
of Chemical Composition (Withdrawn 1996)
teristics similar to the tungsten types.
E527 Practice for Numbering Metals and Alloys in the
NOTE 1—High-speed tool steels are covered in Specification A600.
3.1.2 Cold Work Tool Steels, Identification A—Types A2 to
This specification is under the jurisdiction of ASTM Committee A01 on Steel,
A10 cover a wide range of carbon and alloy contents but all
Stainless Steel and Related Alloysand is the direct responsibility of Subcommittee
have high hardenability and may be hardened in air. The low
A01.29 on Tool Steels.
carbon Types A8 and A9 have less wear resistance but offer
Current edition approved Sept. 1, 2015. Published September 2015. Originally
approved in 1973. Last previous edition approved in 2008 as A681 – 08. DOI:
greater toughness than others in this group.TypeA7, with high
10.1520/A0681-08R15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
Standards volume information, refer to the standard’s Document Summary page on Available from DLA Document Services, Building 4/D, 700 Robbins Ave.,
the ASTM website. Philadelphia, PA 19111-5094, http://quicksearch.dla.mil.
3 5
The last approved version of this historical standard is referenced on Available from SAE International (SAE), 400 Commonwealth Dr.,Warrendale,
www.astm.org. PA 15096, http://www.sae.org.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A681−08 (2015)
carbon and vanadium, offers exceptional wear resistance but at 6.2 Analysis may be made by the purchaser from finished
a very low level of toughness. bars and forgings by machining off the entire cross section and
3.1.3 Cold Work Tool Steels, Identification D—Types D2 to drilling parallel to the axis of the bar or forging at any point
D7 are characterized by high carbon and high chromium midway between the center and surface in accordance with the
contents and exhibit high resistance to abrasion. The types latest issue of Practice E59. The chemical analysis of the
containing molybdenum may be hardened in air and offer a drilling chips shall be made in accordance with the latest issue
high degree of dimensional stability in heat treatment. of Test Methods E30. The chemical composition thus deter-
3.1.4 Cold Work Tool Steels, Identification O—Types O1 to mined shall not vary from the limits specified in Table 1.
O7 are low-alloy types that must be hardened by quenching in
7. Hardness Requirements
oil. Sizes over about 2 in. (50 mm) in cross section usually
exhibit lower interior hardness.
7.1 Annealed hardness values shall be obtained in accor-
3.1.5 Shock-Resisting Steels, Identification S—Types S1 to dance with the latest issue of Test Methods and Definitions
S7 vary in alloy content but are intended for shock-resisting
A370, and shall not exceed the Brinell hardness values (or
applications. equivalent Rockwell hardness values) specified in Table 2.
3.1.6 Special-Purpose Tool Steels, Identification L—Types
7.2 Specimens for determination of minimum response to
L2 to L6 are low-alloy steels with a wide range of carbon
hardening shall be ⁄4-in. (6.4-mm) thick disks cut so as to
content. The low-carbon types are generally used for structural
represent either the full cross-sectional area or that midway
applications requiring good levels of toughness, while the
between the center and outer surface of the material. If the
high-carbon types may be used for short-run tools.
material form or size does not lend itself to accurate hardness
3.1.7 Special-Purpose Tool Steels, Identification F—Types
determination on ⁄4-in. thick cross-sectional disks, then longi-
F1 to F2 are high-carbon steels with varying tungsten content
tudinal specimens may be used for hardness testing. Examples
used primarily for relatively short-run fine edge cutting tools.
are round bars less than ⁄2 in. (12.7 mm) in diameter or sheet.
3.1.8 Mold Steels, Identification P:
In this case, the specimen shall be a minimum of 3 in. (76 mm)
3.1.8.1 Types P2 to P6 are very low-carbon steels and must
in length and parallel flats shall be ground on the original mill
be carburized after machining or hubbing.
surfaces. The specimens shall be heat treated as prescribed in
3.1.8.2 Types P20 and P21 are usually supplied in the
Table 3.
prehardened condition and can be placed in service directly
7.2.1 The hardness of the specimen after the specified heat
after machining.
treatment shall meet the minimum hardness value for the
particular type of steel shown in Table 3. Rockwell C tests
4. Ordering Information
should be used where possible but light load tests may be
4.1 Orders for material under this specification shall include
necessaryonthinspecimens.Thesetestsshouldbespecifiedby
the following information, as required to describe adequately
agreement between the seller and the purchaser. The hardness
the desired material:
value shall be obtained in accordance with the latest issue of
4.1.1 Class of material (hot work tool steel, etc.),
TestMethodsandDefinitionsA370,andshallbetheaverageof
4.1.2 Type (H11, D2, etc.),
at least five readings taken in an area midway between the
4.1.3 Shape (sheet, strip, plate, flat bar, round bar, square
center and surface of the largest dimension of the cross-
bar, hexagon bar, octagon, special shapes),
sectional specimen or along the parallel surfaces of the
4.1.4 Dimensions (thickness, width, diameter, length),
longitudinal specimen.
4.1.5 Finish (hot rolled, forged, blasted or pickled, cold
8. Macrostructure
drawn, machined, ground, precision ground and polished),
4.1.6 Condition (annealed, hardened and tempered, etc.),
8.1 Specimens for the determination of the macrostructure
4.1.7 ASTM designation and year of issue, and
shall represent the entire cross-sectional area in the annealed
4.1.8 Special requirements.
conditionandbepreparedinaccordancewiththelatestissueof
Practice A561. Material supplied to this specification shall be
5. Materials and Manufacture
capable of exhibiting a structure free of excessive porosity,
segregation, slag, dirt or other nonmetallic inclusions, pipe,
5.1 Unless otherwise specified, material covered by this
checks, cracks, and other injurious defects.
specification shall be made by an electric melting process. It
shall be made from ingots or slabs that have been reduced in
8.2 Macroetch severity levels for center porosity and ingot
crosssectioninsuchamannerandtosuchadegreeastoensure
pattern, illustrated photographically in Practice A561, shall not
proper refinement of the solidification structure.
exceed the ratings specification in Table 4 for the appropriate
materialsizeandcomposition.Morestringentrequirementsare
6. Chemical Composition
available by agreement between seller and purchaser.
6.1 An analysis of each heat of steel shall be made by the
9. Decarburization
manufacturer to determine the percentage of the elements
specified, and these values shall conform to the requirements 9.1 Specimens for the determination of decarburization
for chemical composition specified in Table 1. If requested or shall represent a cross section of the material and be prepared
required, the chemical composition shall be reported to the in accordance with the latest issue of Guide E3. Material
purchaser or his representative. supplied to this specification shall be capable, when examined
A681−08 (2015)
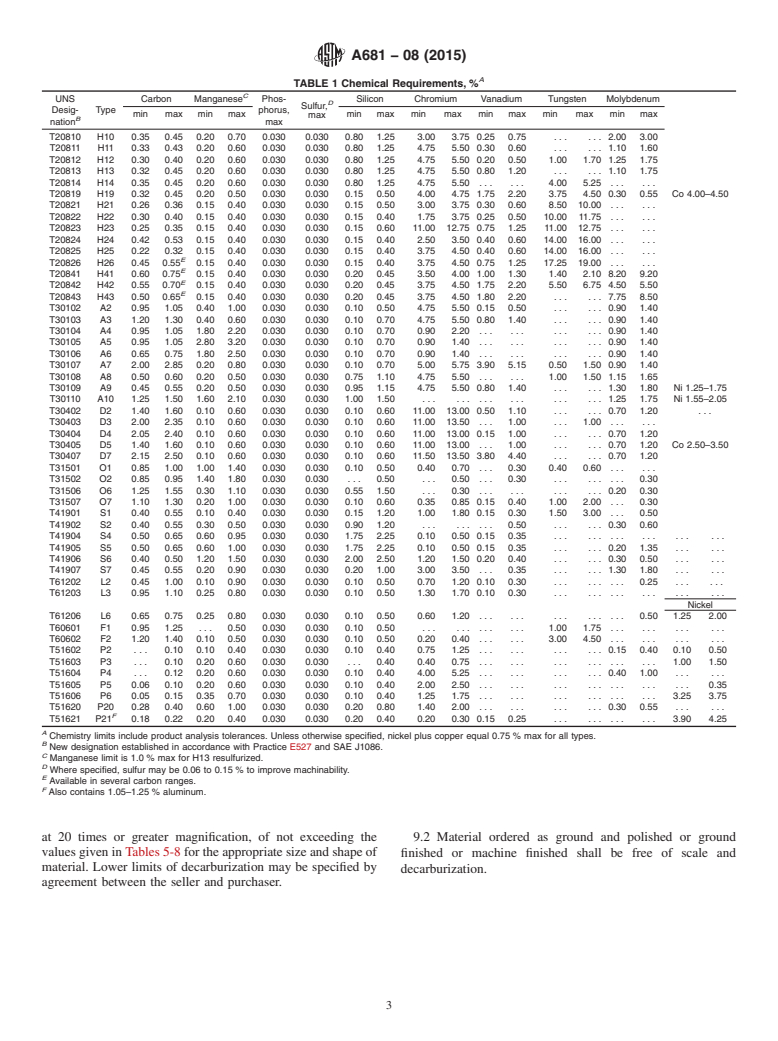
A
TABLE 1 Chemical Requirements,%
C
UNS Carbon Manganese Phos- Silicon Chromium Vanadium Tungsten Molybdenum
D
Sulfur,
Desig- Type phorus,
min max min max max min max min max min max min max min max
B
nation max
T20810 H10 0.35 0.45 0.20 0.70 0.030 0.030 0.80 1.25 3.00 3.75 0.25 0.75 . . . . . . 2.00 3.00
T20811 H11 0.33 0.43 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.30 0.60 . . . . . . 1.10 1.60
T20812 H12 0.30 0.40 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.20 0.50 1.00 1.70 1.25 1.75
T20813 H13 0.32 0.45 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.80 1.20 . . . . . . 1.10 1.75
T20814 H14 0.35 0.45 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 . . . . . . 4.00 5.25 . . . . . .
T20819 H19 0.32 0.45 0.20 0.50 0.030 0.030 0.15 0.50 4.00 4.75 1.75 2.20 3.75 4.50 0.30 0.55 Co 4.00–4.50
T20821 H21 0.26 0.36 0.15 0.40 0.030 0.030 0.15 0.50 3.00 3.75 0.30 0.60 8.50 10.00 . . . . . .
T20822 H22 0.30 0.40 0.15 0.40 0.030 0.030 0.15 0.40 1.75 3.75 0.25 0.50 10.00 11.75 . . . . . .
T20823 H23 0.25 0.35 0.15 0.40 0.030 0.030 0.15 0.60 11.00 12.75 0.75 1.25 11.00 12.75 . . . . . .
T20824 H24 0.42 0.53 0.15 0.40 0.030 0.030 0.15 0.40 2.50 3.50 0.40 0.60 14.00 16.00 . . . . . .
T20825 H25 0.22 0.32 0.15 0.40 0.030 0.030 0.15 0.40 3.75 4.50 0.40 0.60 14.00 16.00 . . . . . .
E
T20826 H26 0.45 0.55 0.15 0.40 0.030 0.030 0.15 0.40 3.75 4.50 0.75 1.25 17.25 19.00 . . . . . .
E
T20841 H41 0.60 0.75 0.15 0.40 0.030 0.030 0.20 0.45 3.50 4.00 1.00 1.30 1.40 2.10 8.20 9.20
E
T20842 H42 0.55 0.70 0.15 0.40 0.030 0.030 0.20 0.45 3.75 4.50 1.75 2.20 5.50 6.75 4.50 5.50
E
T20843 H43 0.50 0.65 0.15 0.40 0.030 0.030 0.20 0.45 3.75 4.50 1.80 2.20 . . . . . . 7.75 8.50
T30102 A2 0.95 1.05 0.40 1.00 0.030 0.030 0.10 0.50 4.75 5.50 0.15 0.50 . . . . . . 0.90 1.40
T30103 A3 1.20 1.30 0.40 0.60 0.030 0.030 0.10 0.70 4.75 5.50 0.80 1.40 . . . . . . 0.90 1.40
T30104 A4 0.95 1.05 1.80 2.20 0.030 0.030 0.10 0.70 0.90 2.20 . . . . . . . . . . . . 0.90 1.40
T30105 A5 0.95 1.05 2.80 3.20 0.030 0.030 0.10 0.70 0.90 1.40 . . . . . . . . . . . . 0.90 1.40
T30106 A6 0.65 0.75 1.80 2.50 0.030 0.030 0.10 0.70 0.90 1.40 . . . . . . . . . . . . 0.90 1.40
T30107 A7 2.00 2.85 0.20 0.80 0.030 0.030 0.10 0.70 5.00 5.75 3.90 5.15 0.50 1.50 0.90 1.40
T30108 A8 0.50 0.60 0.20 0.50 0.030 0.030 0.75 1.10 4.75 5.50 . . . . . . 1.00 1.50 1.15 1.65
T30109 A9 0.45 0.55 0.20 0.50 0.030 0.030 0.95 1.15 4.75 5.50 0.80 1.40 . . . . . . 1.30 1.80 Ni 1.25–1.75
T30110 A10 1.25 1.50 1.60 2.10 0.030 0.030 1.00 1.50 . . . . . . . . . . . . . . . . . . 1.25 1.75 Ni 1.55–2.05
T30402 D2 1.40 1.60 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.00 0.50 1.10 . . . . . . 0.70 1.20 . . .
T30403 D3 2.00 2.35 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.50 . . . 1.00 . . . 1.00 . . . . . .
T30404 D4 2.05 2.40 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.00 0.15 1.00 . . . . . . 0.70 1.20
T30405 D5 1.40 1.60 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.00 . . . 1.00 . . . . . . 0.70 1.20 Co 2.50–3.50
T30407 D7 2.15 2.50 0.10 0.60 0.030 0.030 0.10 0.60 11.50 13.50 3.80 4.40 . . . . . . 0.70 1.20
T31501 O1 0.85 1.00 1.00 1.40 0.030 0.030 0.10 0.50 0.40 0.70 . . . 0.30 0.40 0.60 . . . . . .
T31502 O2 0.85 0.95 1.40 1.80 0.030 0.030 . . . 0.50 . . . 0.50 . . . 0.30 . . . . . . . . . 0.30
T31506 O6 1.25 1.55 0.30 1.10 0.030 0.030 0.55 1.50 . . . 0.30 . . . . . . . . . . . . 0.20 0.30
T31507 O7 1.10 1.30 0.20 1.00 0.030 0.030 0.10 0.60 0.35 0.85 0.15 0.40 1.00 2.00 . . . 0.30
T41901 S1 0.40 0.55 0.10 0.40 0.030 0.030 0.15 1.20 1.00 1.80 0.15 0.30 1.50 3.00 . . . 0.50
T41902 S2 0.40 0.55 0.30 0.50 0.030 0.030 0.90 1.20 . . . . . . . . . 0.50 . . . . . . 0.30 0.60
T41904 S4 0.50 0.65 0.60 0.95 0.030 0.030 1.75 2.25 0.10 0.50 0.15 0.35 . . . . . . . . . . . . . . . . . .
T41905 S5 0.50 0.65 0.60 1.00 0.030 0.030 1.75 2.25 0.10 0.50 0.15 0.35 . . . . . . 0.20 1.35 . . . . . .
T41906 S6 0.40 0.50 1.20 1.50 0.030 0.030 2.00 2.50 1.20 1.50 0.20 0.40 . . . . . . 0.30 0.50 . . . . . .
T41907 S7 0.45 0.55 0.20 0.90 0.030 0.030 0.20 1.00 3.00 3.50 . . . 0.35 . . . . . . 1.30 1.80 . . . . . .
T61202 L2 0.45 1.00 0.10 0.90 0.030 0.030 0.10 0.50 0.70 1.20 0.10 0.30 . . . . . . . . . 0.25 . . . . . .
T61203 L3 0.95 1.10 0.25 0.80 0.030 0.030 0.10 0.50 1.30 1.70 0.10 0.30 . . . . . . . . . . . . . . . .
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: A681 − 08 A681 − 08 (Reapproved 2015)
Standard Specification for
Tool Steels Alloy
This standard is issued under the fixed designation A681; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope
1.1 This specification covers the chemical, mechanical, and physical requirements for available wrought alloy tool steel
products.
1.2 These products, which include hot or cold finished bar, plate, sheet, strip, rod, wire, or forgings, are normally fabricated into
tools, dies, or fixtures. The selection of a material for a particular application will depend upon design, service conditions, and
desired properties.
1.3 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are mathematical
conversions to SI units that are provided for information only and are not considered standard.
2. Referenced Documents
2.1 ASTM Standards:
A370 Test Methods and Definitions for Mechanical Testing of Steel Products
A561 Practice for Macroetch Testing of Tool Steel Bars
A600 Specification for Tool Steel High Speed
A700 Guide for Packaging, Marking, and Loading Methods for Steel Products for Shipment
E3 Guide for Preparation of Metallographic Specimens
E30 Test Methods for Chemical Analysis of Steel, Cast Iron, Open-Hearth Iron, and Wrought Iron (Withdrawn 1995)
E45 Test Methods for Determining the Inclusion Content of Steel
E59 Practice for Sampling Steel and Iron for Determination of Chemical Composition (Withdrawn 1996)
E527 Practice for Numbering Metals and Alloys in the Unified Numbering System (UNS)
2.2 Military Standard:
MIL-STD-163 Steel Mill Products, Preparation for Shipment and Storage
2.3 Federal Standards:
Fed. Std. No. 123 Marking and Shipment (Civil Agencies)
Fed. Std. No. 183 Continuous Identification Marking of Iron and Steel Products
2.4 Other Standards:
SAE J1086 Recommended Practice for Numbering Metals and Alloys (UNS)
3. Classification
3.1 Material in accordance with this specification is classified by chemical composition. Types correspond to respective AISI
designations.
3.1.1 Hot Work Tool Steels, Identification H:
This specification is under the jurisdiction of ASTM Committee A01 on Steel, Stainless Steel and Related Alloysand is the direct responsibility of Subcommittee A01.29
on Tool Steels.
Current edition approved Oct. 1, 2008Sept. 1, 2015. Published October 2008September 2015. Originally approved in 1973. Last previous edition approved in 20072008
ε1
as A681 – 07A681 – 08. . DOI: 10.1520/A0681-08.10.1520/A0681-08R15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
The last approved version of this historical standard is referenced on www.astm.org.
Available from the Standardization Documents, Order Desk, Bldg. 4, Section DLA Document Services, Building 4/D, 700 D700Robbins Ave.Ave., Philadelphia, PA
19111-5094 Attn: NPODS.19111-5094, http://quicksearch.dla.mil.
Available from the Society of Automotive Engineers, 400 Commonwelth drive, Warrendale, PA 15096.SAE International (SAE), 400 Commonwealth Dr., Warrendale,
PA 15096, http://www.sae.org.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A681 − 08 (2015)
3.1.1.1 Types H10 to H19 are characterized by a controlled chromium content along with other alloying elements. The first four,
containing molybdenum, offer excellent toughness and high hardenability and are frequently used in cold work applications
requiring toughness at relatively high hardness levels.
3.1.1.2 Types H21 to H26 are characterized by a controlled tungsten content along with other alloying elements. These steels
offer greater resistance to the softening effect of elevated service temperatures but exhibit a lower degree of toughness.
3.1.1.3 Types H41 to H43 are low-carbon modifications of molybdenum high speed tool steels (Note 1) and have characteristics
similar to the tungsten types.
NOTE 1—High-speed tool steels are covered in Specification A600.
3.1.2 Cold Work Tool Steels, Identification A—Types A2 to A10 cover a wide range of carbon and alloy contents but all have
high hardenability and may be hardened in air. The low carbon Types A8 and A9 have less wear resistance but offer greater
toughness than others in this group. Type A7, with high carbon and vanadium, offers exceptional wear resistance but at a very low
level of toughness.
3.1.3 Cold Work Tool Steels, Identification D—Types D2 to D7 are characterized by high carbon and high chromium contents
and exhibit high resistance to abrasion. The types containing molybdenum may be hardened in air and offer a high degree of
dimensional stability in heat treatment.
3.1.4 Cold Work Tool Steels, Identification O—Types O1 to O7 are low-alloy types that must be hardened by quenching in oil.
Sizes over about 2 in. (50 mm) in cross section usually exhibit lower interior hardness.
3.1.5 Shock-Resisting Steels, Identification S—Types S1 to S7 vary in alloy content but are intended for shock-resisting
applications.
3.1.6 Special-Purpose Tool Steels, Identification L—Types L2 to L6 are low-alloy steels with a wide range of carbon content.
The low-carbon types are generally used for structural applications requiring good levels of toughness, while the high-carbon types
may be used for short-run tools.
3.1.7 Special-Purpose Tool Steels, Identification F—Types F1 to F2 are high-carbon steels with varying tungsten content used
primarily for relatively short-run fine edge cutting tools.
3.1.8 Mold Steels, Identification P:
3.1.8.1 Types P2 to P6 are very low-carbon steels and must be carburized after machining or hubbing.
3.1.8.2 Types P20 and P21 are usually supplied in the prehardened condition and can be placed in service directly after
machining.
4. Ordering Information
4.1 Orders for material under this specification shall include the following information, as required to describe adequately the
desired material:
4.1.1 Class of material (hot work tool steel, etc.),
4.1.2 Type (H11, D2, etc.),
4.1.3 Shape (sheet, strip, plate, flat bar, round bar, square bar, hexagon bar, octagon, special shapes),
4.1.4 Dimensions (thickness, width, diameter, length),
4.1.5 Finish (hot rolled, forged, blasted or pickled, cold drawn, machined, ground, precision ground and polished),
4.1.6 Condition (annealed, hardened and tempered, etc.),
4.1.7 ASTM designation and year of issue, and
4.1.8 Special requirements.
5. Materials and Manufacture
5.1 Unless otherwise specified, material covered by this specification shall be made by an electric melting process. It shall be
made from ingots or slabs that have been reduced in cross section in such a manner and to such a degree as to ensure proper
refinement of the solidification structure.
6. Chemical Composition
6.1 An analysis of each heat of steel shall be made by the manufacturer to determine the percentage of the elements specified,
and these values shall conform to the requirements for chemical composition specified in Table 1. If requested or required, the
chemical composition shall be reported to the purchaser or his representative.
6.2 Analysis may be made by the purchaser from finished bars and forgings by machining off the entire cross section and drilling
parallel to the axis of the bar or forging at any point midway between the center and surface in accordance with the latest issue
of Practice E59. The chemical analysis of the drilling chips shall be made in accordance with the latest issue of Test Methods E30.
The chemical composition thus determined shall not vary from the limits specified in Table 1.
7. Hardness Requirements
7.1 Annealed hardness values shall be obtained in accordance with the latest issue of Test Methods and Definitions A370, and
shall not exceed the Brinell hardness values (or equivalent Rockwell hardness values) specified in Table 2.
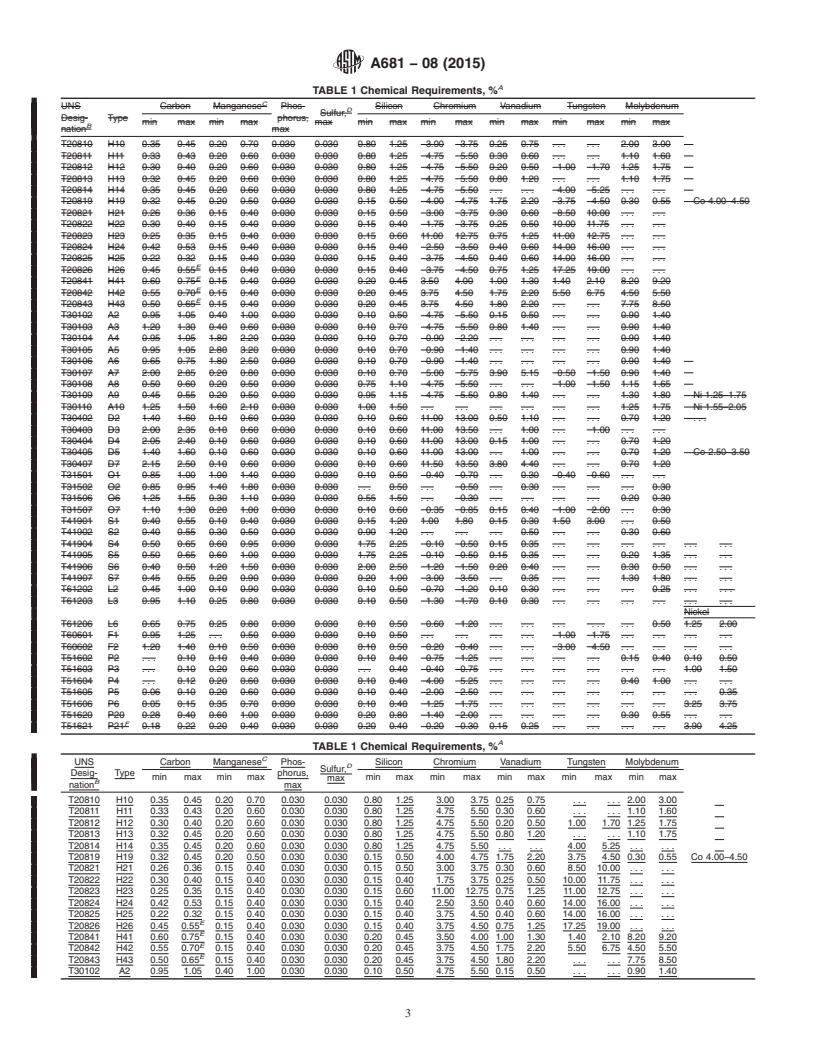
A681 − 08 (2015)
A
TABLE 1 Chemical Requirements, %
C
UNS Carbon Manganese Phos- Silicon Chromium Vanadium Tungsten Molybdenum
D
Sulfur,
Desig- Type phorus,
min max min max max min max min max min max min max min max
B
nation max
T20810 H10 0.35 0.45 0.20 0.70 0.030 0.030 0.80 1.25 3.00 3.75 0.25 0.75 . . . . . . 2.00 3.00
T20811 H11 0.33 0.43 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.30 0.60 . . . . . . 1.10 1.60
T20812 H12 0.30 0.40 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.20 0.50 1.00 1.70 1.25 1.75
T20813 H13 0.32 0.45 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.80 1.20 . . . . . . 1.10 1.75
T20814 H14 0.35 0.45 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 . . . . . . 4.00 5.25 . . . . . .
T20819 H19 0.32 0.45 0.20 0.50 0.030 0.030 0.15 0.50 4.00 4.75 1.75 2.20 3.75 4.50 0.30 0.55 Co 4.00–4.50
T20821 H21 0.26 0.36 0.15 0.40 0.030 0.030 0.15 0.50 3.00 3.75 0.30 0.60 8.50 10.00 . . . . . .
T20822 H22 0.30 0.40 0.15 0.40 0.030 0.030 0.15 0.40 1.75 3.75 0.25 0.50 10.00 11.75 . . . . . .
T20823 H23 0.25 0.35 0.15 0.40 0.030 0.030 0.15 0.60 11.00 12.75 0.75 1.25 11.00 12.75 . . . . . .
T20824 H24 0.42 0.53 0.15 0.40 0.030 0.030 0.15 0.40 2.50 3.50 0.40 0.60 14.00 16.00 . . . . . .
T20825 H25 0.22 0.32 0.15 0.40 0.030 0.030 0.15 0.40 3.75 4.50 0.40 0.60 14.00 16.00 . . . . . .
E
T20826 H26 0.45 0.55 0.15 0.40 0.030 0.030 0.15 0.40 3.75 4.50 0.75 1.25 17.25 19.00 . . . . . .
E
T20841 H41 0.60 0.75 0.15 0.40 0.030 0.030 0.20 0.45 3.50 4.00 1.00 1.30 1.40 2.10 8.20 9.20
E
T20842 H42 0.55 0.70 0.15 0.40 0.030 0.030 0.20 0.45 3.75 4.50 1.75 2.20 5.50 6.75 4.50 5.50
E
T20843 H43 0.50 0.65 0.15 0.40 0.030 0.030 0.20 0.45 3.75 4.50 1.80 2.20 . . . . . . 7.75 8.50
T30102 A2 0.95 1.05 0.40 1.00 0.030 0.030 0.10 0.50 4.75 5.50 0.15 0.50 . . . . . . 0.90 1.40
T30103 A3 1.20 1.30 0.40 0.60 0.030 0.030 0.10 0.70 4.75 5.50 0.80 1.40 . . . . . . 0.90 1.40
T30104 A4 0.95 1.05 1.80 2.20 0.030 0.030 0.10 0.70 0.90 2.20 . . . . . . . . . . . . 0.90 1.40
T30105 A5 0.95 1.05 2.80 3.20 0.030 0.030 0.10 0.70 0.90 1.40 . . . . . . . . . . . . 0.90 1.40
T30106 A6 0.65 0.75 1.80 2.50 0.030 0.030 0.10 0.70 0.90 1.40 . . . . . . . . . . . . 0.90 1.40
T30107 A7 2.00 2.85 0.20 0.80 0.030 0.030 0.10 0.70 5.00 5.75 3.90 5.15 0.50 1.50 0.90 1.40
T30108 A8 0.50 0.60 0.20 0.50 0.030 0.030 0.75 1.10 4.75 5.50 . . . . . . 1.00 1.50 1.15 1.65
T30109 A9 0.45 0.55 0.20 0.50 0.030 0.030 0.95 1.15 4.75 5.50 0.80 1.40 . . . . . . 1.30 1.80 Ni 1.25–1.75
T30110 A10 1.25 1.50 1.60 2.10 0.030 0.030 1.00 1.50 . . . . . . . . . . . . . . . . . . 1.25 1.75 Ni 1.55–2.05
T30402 D2 1.40 1.60 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.00 0.50 1.10 . . . . . . 0.70 1.20 . . .
T30403 D3 2.00 2.35 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.50 . . . 1.00 . . . 1.00 . . . . . .
T30404 D4 2.05 2.40 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.00 0.15 1.00 . . . . . . 0.70 1.20
T30405 D5 1.40 1.60 0.10 0.60 0.030 0.030 0.10 0.60 11.00 13.00 . . . 1.00 . . . . . . 0.70 1.20 Co 2.50–3.50
T30407 D7 2.15 2.50 0.10 0.60 0.030 0.030 0.10 0.60 11.50 13.50 3.80 4.40 . . . . . . 0.70 1.20
T31501 O1 0.85 1.00 1.00 1.40 0.030 0.030 0.10 0.50 0.40 0.70 . . . 0.30 0.40 0.60 . . . . . .
T31502 O2 0.85 0.95 1.40 1.80 0.030 0.030 . . . 0.50 . . . 0.50 . . . 0.30 . . . . . . . . . 0.30
T31506 O6 1.25 1.55 0.30 1.10 0.030 0.030 0.55 1.50 . . . 0.30 . . . . . . . . . . . . 0.20 0.30
T31507 O7 1.10 1.30 0.20 1.00 0.030 0.030 0.10 0.60 0.35 0.85 0.15 0.40 1.00 2.00 . . . 0.30
T41901 S1 0.40 0.55 0.10 0.40 0.030 0.030 0.15 1.20 1.00 1.80 0.15 0.30 1.50 3.00 . . . 0.50
T41902 S2 0.40 0.55 0.30 0.50 0.030 0.030 0.90 1.20 . . . . . . . . . 0.50 . . . . . . 0.30 0.60
T41904 S4 0.50 0.65 0.60 0.95 0.030 0.030 1.75 2.25 0.10 0.50 0.15 0.35 . . . . . . . . . . . . . . . . . .
T41905 S5 0.50 0.65 0.60 1.00 0.030 0.030 1.75 2.25 0.10 0.50 0.15 0.35 . . . . . . 0.20 1.35 . . . . . .
T41906 S6 0.40 0.50 1.20 1.50 0.030 0.030 2.00 2.50 1.20 1.50 0.20 0.40 . . . . . . 0.30 0.50 . . . . . .
T41907 S7 0.45 0.55 0.20 0.90 0.030 0.030 0.20 1.00 3.00 3.50 . . . 0.35 . . . . . . 1.30 1.80 . . . . . .
T61202 L2 0.45 1.00 0.10 0.90 0.030 0.030 0.10 0.50 0.70 1.20 0.10 0.30 . . . . . . . . . 0.25 . . . . . .
T61203 L3 0.95 1.10 0.25 0.80 0.030 0.030 0.10 0.50 1.30 1.70 0.10 0.30 . . . . . . . . . . . . . . . . . .
Nickel
T61206 L6 0.65 0.75 0.25 0.80 0.030 0.030 0.10 0.50 0.60 1.20 . . . . . . . . . . . . . . . 0.50 1.25 2.00
T60601 F1 0.95 1.25 . . . 0.50 0.030 0.030 0.10 0.50 . . . . . . . . . . . . 1.00 1.75 . . . . . . . . . . . .
T60602 F2 1.20 1.40 0.10 0.50 0.030 0.030 0.10 0.50 0.20 0.40 . . . . . . 3.00 4.50 . . . . . . . . . . . .
T51602 P2 . . . 0.10 0.10 0.40 0.030 0.030 0.10 0.40 0.75 1.25 . . . . . . . . . . . . 0.15 0.40 0.10 0.50
T51603 P3 . . . 0.10 0.20 0.60 0.030 0.030 . . . 0.40 0.40 0.75 . . . . . . . . . . . . . . . . . . 1.00 1.50
T51604 P4 . . . 0.12 0.20 0.60 0.030 0.030 0.10 0.40 4.00 5.25 . . . . . . . . . . . . 0.40 1.00 . . . . . .
T51605 P5 0.06 0.10 0.20 0.60 0.030 0.030 0.10 0.40 2.00 2.50 . . . . . . . . . . . . . . . . . . . . . 0.35
T51606 P6 0.05 0.15 0.35 0.70 0.030 0.030 0.10 0.40 1.25 1.75 . . . . . . . . . . . . . . . . . . 3.25 3.75
T51620 P20 0.28 0.40 0.60 1.00 0.030 0.030 0.20 0.80 1.40 2.00 . . . . . . . . . . . . 0.30 0.55 . . . . . .
F
T51621 P21 0.18 0.22 0.20 0.40 0.030 0.030 0.20 0.40 0.20 0.30 0.15 0.25 . . . . . . . . . . . . 3.90 4.25
A
TABLE 1 Chemical Requirements, %
C
UNS Carbon Manganese Phos- Silicon Chromium Vanadium Tungsten Molybdenum
D
Sulfur,
Desig- Type phorus,
min max min max max min max min max min max min max min max
B
nation max
T20810 H10 0.35 0.45 0.20 0.70 0.030 0.030 0.80 1.25 3.00 3.75 0.25 0.75 . . . . . . 2.00 3.00
T20811 H11 0.33 0.43 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.30 0.60 . . . . . . 1.10 1.60
T20812 H12 0.30 0.40 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.20 0.50 1.00 1.70 1.25 1.75
T20813 H13 0.32 0.45 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 0.80 1.20 . . . . . . 1.10 1.75
T20814 H14 0.35 0.45 0.20 0.60 0.030 0.030 0.80 1.25 4.75 5.50 . . . . . . 4.00 5.25 . . . . . .
T20819 H19 0.32 0.45
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.