


ASTM A1033-10(2015)
(Practice)Standard Practice for Quantitative Measurement and Reporting of Hypoeutectoid Carbon and Low-Alloy Steel Phase Transformations
Standard Practice for Quantitative Measurement and Reporting of Hypoeutectoid Carbon and Low-Alloy Steel Phase Transformations
SIGNIFICANCE AND USE
5.1 This practice is used to provide steel phase transformation data required for use in numerical models for the prediction of microstructures, properties, and distortion during steel manufacturing, forging, casting, heat treatment, and welding. Alternatively, the practice provides end users of steel and fabricated steel products the phase transformation data required for selecting steel grades for a given application by determining the microstructure resulting from a prescribed thermal cycle.
5.1.1 There are available several computer models designed to predict the microstructures, mechanical properties, and distortion of steels as a function of thermal processing cycle. Their use is predicated on the availability of accurate and consistent thermal and transformation strain data. Strain, both thermal and transformation, developed during thermal cycling is the parameter used in predicting both microstructure and properties, and for estimating distortion. It should be noted that these models are undergoing continued development. This process is aimed, among other things, at establishing a direct link between discrete values of strain and specific microstructure constituents in steels. This practice describes a standardized method for measuring strain during a defined thermal cycle.
5.1.2 This practice is suitable for providing data for computer models used in the control of steel manufacturing, forging, casting, heat-treating, and welding processes. It is also useful in providing data for the prediction of microstructures and properties to assist in steel alloy selection for end-use applications.
5.1.3 This practice is suitable for providing the data needed for the construction of transformation diagrams that depict the microstructures developed during the thermal processing of steels as functions of time and temperature. Such diagrams provide a qualitative assessment of the effects of changes in thermal cycle on steel microstructure. Appendix X2 describes ...
SCOPE
1.1 This practice covers the determination of hypoeutectoid steel phase transformation behavior by using high-speed dilatometry techniques for measuring linear dimensional change as a function of time and temperature, and reporting the results as linear strain in either a numerical or graphical format.
1.2 The practice is applicable to high-speed dilatometry equipment capable of programmable thermal profiles and with digital data storage and output capability.
1.3 This practice is applicable to the determination of steel phase transformation behavior under both isothermal and continuous cooling conditions.
1.4 This practice includes requirements for obtaining metallographic information to be used as a supplement to the dilatometry measurements.
1.5 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.6 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: A1033 − 10 (Reapproved 2015)
Standard Practice for
Quantitative Measurement and Reporting of Hypoeutectoid
Carbon and Low-Alloy Steel Phase Transformations
This standard is issued under the fixed designation A1033; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope* 3. Terminology
3.1 Definitions of Terms Specific to This Standard:
1.1 This practice covers the determination of hypoeutectoid
steel phase transformation behavior by using high-speed 3.1.1 diametrical linear engineering strain—the strain, ei-
dilatometry techniques for measuring linear dimensional ther thermal or resulting from phase transformation, that is
changeasafunctionoftimeandtemperature,andreportingthe determined from a change in diameter as a result of a change
resultsaslinearstrainineitheranumericalorgraphicalformat. intemperature,oroveraperiodoftime,andwhichisexpressed
as follows:
1.2 The practice is applicable to high-speed dilatometry
e 5∆d/d 5 d 2 d /d
equipment capable of programmable thermal profiles and with ~ !
D 0 1 0 0
digital data storage and output capability.
3.1.2 hypoeutectoid steel—a term used to describe a group
of carbon steels with a carbon content less than the eutectoid
1.3 This practice is applicable to the determination of steel
composition (0.8% by weight).
phase transformation behavior under both isothermal and
continuous cooling conditions. 3.1.3 longitudinal linear engineering strain—the strain, ei-
ther thermal or resulting from phase transformation, that is
1.4 This practice includes requirements for obtaining met-
determined from a change in length as a result of a change in
allographic information to be used as a supplement to the
temperature, or over a period of time, and which is expressed
dilatometry measurements.
as follows:
1.5 The values stated in SI units are to be regarded as
e 5∆l/L 5 l 2 l /l
~ !
L 0 1 0 0
standard. No other units of measurement are included in this
3.1.4 steel phase transformation—during heating, the crys-
standard.
tallographic transformation from ferrite, pearlite, bainite, mar-
1.6 This standard does not purport to address all of the
tensite or combinations of these constituents to austenite.
safety concerns, if any, associated with its use. It is the
During cooling, the crystallographic transformation from aus-
responsibility of the user of this standard to establish appro-
tenitetoferrite,pearlite,bainite,ormartensiteoracombination
priate safety and health practices and determine the applica-
thereof.
bility of regulatory limitations prior to use.
3.1.5 volumetric engineering strain—the strain, either ther-
mal or resulting from phase transformation, that is determined
2. Referenced Documents
fromachangeinvolumeasaresultofachangeintemperature,
2.1 ASTM Standards:
or over a period of time, and which is expressed as follows:
E3Guide for Preparation of Metallographic Specimens
e 5∆v/v 5 ~v 2 v !/v
V 0 1 0 0
E112Test Methods for Determining Average Grain Size
e '3e '3e
V L D
E407Practice for Microetching Metals and Alloys
3.2 Symbols:
e =longitudinal linear engineering strain
L
e =diametrical linear engineering strain
1 D
This practice is under the jurisdiction of ASTM Committee A01 on Steel,
e =volumetric engineering strain
Stainless Steel and RelatedAlloys and is the direct responsibility of Subcommittee
V
A01.13 on Mechanical and Chemical Testing and Processing Methods of Steel
∆l=change in test specimen length
Products and Processes.
l =test specimen length at specific temperature or time, or
Current edition approved March 1, 2015. Published March 2015. Originally
both
approved in 2004. Last previous edition approved in 2010 as A1033–10. DOI:
10.1520/A1033-10R15.
l =initial test specimen length
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
∆d=change in test specimen diameter
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
d =test specimen diameter at specific temperature or time,
Standards volume information, refer to the standard’s Document Summary page on 1
the ASTM website. or both
*A Summary of Changes section appears at the end of this standard
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A1033 − 10 (2015)
d =initial test specimen diameter steels as functions of time and temperature. Such diagrams
∆v=change in test specimen volume provide a qualitative assessment of the effects of changes in
v =test specimen volume at a specific temperature or time, thermal cycle on steel microstructure. Appendix X2 describes
or both construction of these diagrams.
v =initial test specimen volume
5.2 It should be recognized that thermal and transformation
Ac =the temperature at which austenite begins to form on
strains, which develop in steels during thermal cycling, are
heating
sensitive to chemical composition. Thus, anisotropy in chemi-
Ac =the temperature at which the transformation of ferrite
calcompositioncanresultinvariabilityinstrain,andcanaffect
to austenite is complete on heating
theresultsofstraindeterminations,especiallydeterminationof
M =the temperature at which the transformation of austen-
s
volumetric strain. Strains determined during cooling are sen-
ite to martensite starts during cooling
sitive to the grain size of austenite, which is determined by the
heating cycle. The most consistent results are obtained when
4. Summary of Practice
austenitegrainsizeismaintainedbetweenASTMgrainsizesof
4.1 This practice is based upon the principle that, during
5to8.Finally,theeutectoidcarboncontentisdefinedas0.8%
heating and cooling of steels, dimensional changes occur as a
for carbon steels. Additions of alloying elements can change
result of both thermal expansion associated with temperature
this value, along with Ac and Ac temperatures. Heating
1 3
change and phase transformation. In this practice, sensitive
cycles need to be employed, as described below, to ensure
high-speed dilatometer equipment is used to detect and mea-
completeformationofausteniteprecedingstrainmeasurements
sure the changes in dimension that occur as functions of both
during cooling.
time and temperature during defined thermal cycles. The
resulting data are converted to discrete values of strain for
6. Ordering Information
specific values of time and temperature during the thermal
6.1 When this practice is to be applied to an inquiry,
cycle. Strain as a function of time or temperature, or both, can
contract, or order, the purchaser shall so state and should
thenbeusedtodeterminethebeginningandcompletionofone
furnish the following information:
or more phase transformations.
6.1.1 The steel grades to be evaluated,
5. Significance and Use
6.1.2 The test apparatus to be used,
6.1.3 The specimen configuration and dimensions to be
5.1 This practice is used to provide steel phase transforma-
used,
tion data required for use in numerical models for the predic-
6.1.4 The thermal cycles to be used, and
tion of microstructures, properties, and distortion during steel
6.1.5 The supplementary requirements desired.
manufacturing, forging, casting, heat treatment, and welding.
Alternatively, the practice provides end users of steel and
7. Apparatus
fabricatedsteelproductsthephasetransformationdatarequired
for selecting steel grades for a given application by determin- 7.1 This practice is applicable to several types of commer-
cially available high-speed dilatometer apparatus, which have
ing the microstructure resulting from a prescribed thermal
cycle. certain common features. These include the capabilities for:
heating and cooling a steel specimen in vacuum or other
5.1.1 Thereareavailableseveralcomputermodelsdesigned
to predict the microstructures, mechanical properties, and controlledatmosphere;programmablethermalcycles;inertgas
or liquid injection for rapid cooling; continuous measurement
distortion of steels as a function of thermal processing cycle.
Their use is predicated on the availability of accurate and of specimen dimension and temperature; and digital data
storage and output. The apparatus differ in terms of method of
consistent thermal and transformation strain data. Strain, both
specimen heating and test specimen design.
thermal and transformation, developed during thermal cycling
7.1.1 DilatometerApparatus Using Induction Heating—The
is the parameter used in predicting both microstructure and
test specimen is heated by suspending it inside an induction-
properties,andforestimatingdistortion.Itshouldbenotedthat
heating coil between two platens as shown schematically in
these models are undergoing continued development. This
Fig.1.Coolingisaccomplishedbyacombinationofcontrolled
process is aimed, among other things, at establishing a direct
link between discrete values of strain and specific microstruc- reduction in heating current along with injection of inert gas
onto the test specimen. Dimensional change is measured by a
ture constituents in steels. This practice describes a standard-
ized method for measuring strain during a defined thermal mechanical apparatus along the longitudinal axis of the test
specimen, and temperature is measured by a thermocouple
cycle.
5.1.2 This practice is suitable for providing data for com- welded to the surface of the specimen at the center of the
specimen length. For this apparatus, only Type R or S
puter models used in the control of steel manufacturing,
forging,casting,heat-treating,andweldingprocesses.Itisalso thermocouples should be used.
useful in providing data for the prediction of microstructures
and properties to assist in steel alloy selection for end-use
applications.
5.1.3 This practice is suitable for providing the data needed
for the construction of transformation diagrams that depict the
microstructures developed during the thermal processing of
A1033 − 10 (2015)
FIG. 1 Schematic of Transformation Testing Using Induction Heating
7.1.2 Dilatometer Apparatus Using Resistance Heating — 8.1.1 Dilatometers Apparatus Using Induction Heating—
The test specimen is supported between two grips as shown Thespecimenstobeusedwiththistypeofapparatusareshown
schematicallyinFig.2,andheatedbydirectresistanceheating. in Fig. 3. The solid specimens may be used for all thermal
Cooling is accomplished by a combination of controlled cyclingconditions.Thehollowspecimensmayalsobeusedfor
reduction in heating current along with injection of inert gas all thermal cycling conditions. The hollow specimens will
onto the test specimen or internal liquid quenching. Dimen- achieve the highest cooling rates when gas quenching is
sionalchangeismeasuredalongadiameteratthecenterofthe employed.
test specimen length, and temperature is measured by a
8.1.2 Dilatometer Apparatus Using Resistance Heating —
thermocouple welded to the surface of the specimen at the
Thespecimensforusewiththistypeofapparatusareshownin
center of the specimen length. Dimensional change can be
Figs. 4 and 5. The specimen with the reduced center section
measured by either mechanical or non-contact (laser) dimen-
(Fig. 4) allows for internal cooling of the specimen ends by
sion measuring apparatus. Temperature measurement can be
eitherliquidorgas.ThesolidspecimenshowninFig.5maybe
made using Type K, Type R, or Type S thermocouples.
used for all thermal cycling conditions. The hollow specimen
shown in Fig. 5 may also be used for all thermal cycling
8. Test Specimens and Sampling of Test Specimens
conditions. The hollow specimens will achieve the highest
8.1 Test Specimens—The test specimens to be used with
cooling rates when quenching is employed.
eachtypeoftestequipmentshallbeselectedfromthoseshown
8.2 Sampling—Test specimens may be obtained from any
in Figs. 3-5.
steel product form, including steel bar, plate, and sheet and
strip products. Care should be exercised to avoid the effects of
Thesolesourceofsupplyoftheapparatusknowntothecommitteeatthistime metallurgical variables, such as chemical segregation, in deter-
is Dynamic Systems Incorporated, Postenkill, NY. If you are aware of alternative
miningwheretestspecimensareobtainedfromaproductform.
suppliers, please provide this information to ASTM International Headquarters.
Procedures have been designed that offer the advantage of
Your comments will receive careful consideration at a meeting of the responsible
equivalencyofstraindeterminationusingspecimensfromboth
technical committee , which you may attend.
FIG. 2 Schematic of Transformation Testing Using Resistance Heating
A1033 − 10 (2015)
NOTE 1—All machining surface finishes being 0.8 µm RMS
FIG. 3 Test Specimens for Induction Heating Apparatus
NOTE 1—All machining surface finishes being 0.8 µm RMS
Test Specimen Dimension Guide Table
Reduced Section
Specimen Length, Specimen Half Length, Reduced Section Diameter, OD at Grip End, ID at Grip End, Grip End Drill Depth,
Length,
L1±0.10(mm) L2±0.05(mm) D3 ± 0.025 (mm) D1 ± 0.025 (mm) D2 ± 0.025 (mm) L4±0.05(mm)
L3 ± 0.025 (mm)
90 45 6 6 10 6.3 40
84 42 6 6 10 6.3 37
84 42 5 5 10 6.3 37
FIG. 4 Test Specimens with Reduced Center Section for Resistance Heating Apparatus
types of apparatus described in 7.1.1 and 7.1.2. For equiva- 8.2.1 Example Sampling for Steel Bar Product Forms—
lency of strain, the orientation of the longitudinal axis of test Where material thickness permits, a selected test specimen
specimens for induction heating apparatus should be at 90 should be machined from the mid-radius position. Where
degrees to the longitudinal axis of specimens for resistance materialthicknessisinsufficienttopermitmachiningaselected
heating. test specimen from the mid-radius position but sufficient to
A1033 − 10 (2015)
NOTE 1—All machining surface finishes being 0.8 µm RMS.
Test Specimen Dimension Guide Table
Reduced Section
Specimen Length, Specimen Half Length, Reduced Section Diameter, OD at Grip End, ID at Grip End, Grip End Drill Depth,
Length,
L1±0.10(mm) L2±0.05(mm) D3 ± 0.025 (mm) D1 ± 0.025 (mm) D2 ± 0.025 (mm) L4±0.05(mm)
L3 ± 0.025 (mm)
90 45 6 6 10 6.3 40
84 42 6 6 10 6.3 37
84 42 5 5 10 6.3 37
FIG. 5 Test Specimens for Resistance Heating Apparatus
permit machining the test specimen from the mid-diameter nominal rate of 1°C/s, held at temperature for 60 s and then
position, the test specimen may be obtained from the mid- cooled at a nominal rate of 1°C/s to room temperature. Thi
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: A1033 − 10 A1033 − 10 (Reapproved 2015)
Standard Practice for
Quantitative Measurement and Reporting of Hypoeutectoid
Carbon and Low-Alloy Steel Phase Transformations
This standard is issued under the fixed designation A1033; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope*
1.1 This practice covers the determination of hypoeutectoid steel phase transformation behavior by using high-speed
dilatometry techniques for measuring linear dimensional change as a function of time and temperature, and reporting the results
as linear strain in either a numerical or graphical format.
1.2 The practice is applicable to high-speed dilatometry equipment capable of programmable thermal profiles and with digital
data storage and output capability.
1.3 This practice is applicable to the determination of steel phase transformation behavior under both isothermal and continuous
cooling conditions.
1.4 This practice includes requirements for obtaining metallographic information to be used as a supplement to the dilatometry
measurements.
1.5 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.6 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory
limitations prior to use.
2. Referenced Documents
2.1 ASTM Standards:
E3 Guide for Preparation of Metallographic Specimens
E112 Test Methods for Determining Average Grain Size
E407 Practice for Microetching Metals and Alloys
3. Terminology
3.1 Definitions of Terms Specific to This Standard:
3.1.1 diametrical linear engineering strain—the strain, either thermal or resulting from phase transformation, that is determined
from a change in diameter as a result of a change in temperature, or over a period of time, and which is expressed as follows:
e 5 Δd/d 5 ~d 2 d !/d
D 0 1 0 0
3.1.2 hypoeutectoid steel—a term used to describe a group of carbon steels with a carbon content less than the eutectoid
composition (0.8 % by weight).
3.1.3 longitudinal linear engineering strain—the strain, either thermal or resulting from phase transformation, that is determined
from a change in length as a result of a change in temperature, or over a period of time, and which is expressed as follows:
e 5 Δl/L 5 l 2 l /l
~ !
L 0 1 0 0
3.1.4 steel phase transformation—during heating, the crystallographic transformation from ferrite, pearlite, bainite, martensite
or combinations of these constituents to austenite. During cooling, the crystallographic transformation from austenite to ferrite,
pearlite, bainite, or martensite or a combination thereof.
This practice is under the jurisdiction of ASTM Committee A01 on Steel, Stainless Steel and Related Alloys and is the direct responsibility of Subcommittee A01.13
on Mechanical and Chemical Testing and Processing Methods of Steel Products and Processes.
Current edition approved April 1, 2010March 1, 2015. Published April 2010March 2015. Originally approved in 2004. Last previous edition approved in 20042010 as
A1033 – 04.A1033 – 10. DOI: 10.1520/A1033-10.10.1520/A1033-10R15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
*A Summary of Changes section appears at the end of this standard
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A1033 − 10 (2015)
3.1.5 volumetric engineering strain—the strain, either thermal or resulting from phase transformation, that is determined from
a change in volume as a result of a change in temperature, or over a period of time, and which is expressed as follows:
e 5 Δv/v 5 v 2 v /v
~ !
V 0 1 0 0
e '3e '3e
V L D
3.2 Symbols:
e = longitudinal linear engineering strain
L
e = diametrical linear engineering strain
D
e = volumetric engineering strain
V
Δl = change in test specimen length
l = test specimen length at specific temperature or time, or both
l = initial test specimen length
Δd = change in test specimen diameter
d = test specimen diameter at specific temperature or time, or both
d = initial test specimen diameter
Δv = change in test specimen volume
v = test specimen volume at a specific temperature or time, or both
v = initial test specimen volume
Ac = the temperature at which austenite begins to form on heating
Ac = the temperature at which the transformation of ferrite to austenite is complete on heating
M = the temperature at which the transformation of austenite to martensite starts during cooling
s
4. Summary of Practice
4.1 This practice is based upon the principle that, during heating and cooling of steels, dimensional changes occur as a result
of both thermal expansion associated with temperature change and phase transformation. In this practice, sensitive high-speed
dilatometer equipment is used to detect and measure the changes in dimension that occur as functions of both time and temperature
during defined thermal cycles. The resulting data are converted to discrete values of strain for specific values of time and
temperature during the thermal cycle. Strain as a function of time or temperature, or both, can then be used to determine the
beginning and completion of one or more phase transformations.
5. Significance and Use
5.1 This practice is used to provide steel phase transformation data required for use in numerical models for the prediction of
microstructures, properties, and distortion during steel manufacturing, forging, casting, heat treatment, and welding. Alternatively,
the practice provides end users of steel and fabricated steel products the phase transformation data required for selecting steel
grades for a given application by determining the microstructure resulting from a prescribed thermal cycle.
5.1.1 There are available several computer models designed to predict the microstructures, mechanical properties, and distortion
of steels as a function of thermal processing cycle. Their use is predicated on the availability of accurate and consistent thermal
and transformation strain data. Strain, both thermal and transformation, developed during thermal cycling is the parameter used
in predicting both microstructure and properties, and for estimating distortion. It should be noted that these models are undergoing
continued development. This process is aimed, among other things, at establishing a direct link between discrete values of strain
and specific microstructure constituents in steels. This practice describes a standardized method for measuring strain during a
defined thermal cycle.
5.1.2 This practice is suitable for providing data for computer models used in the control of steel manufacturing, forging,
casting, heat-treating, and welding processes. It is also useful in providing data for the prediction of microstructures and properties
to assist in steel alloy selection for end-use applications.
5.1.3 This practice is suitable for providing the data needed for the construction of transformation diagrams that depict the
microstructures developed during the thermal processing of steels as functions of time and temperature. Such diagrams provide
a qualitative assessment of the effects of changes in thermal cycle on steel microstructure. Appendix X2 describes construction of
these diagrams.
5.2 It should be recognized that thermal and transformation strains, which develop in steels during thermal cycling, are sensitive
to chemical composition. Thus, anisotropy in chemical composition can result in variability in strain, and can affect the results of
strain determinations, especially determination of volumetric strain. Strains determined during cooling are sensitive to the grain
size of austenite, which is determined by the heating cycle. The most consistent results are obtained when austenite grain size is
maintained between ASTM grain sizes of 5 to 8. Finally, the eutectoid carbon content is defined as 0.8 % for carbon steels.
Additions of alloying elements can change this value, along with Ac and Ac temperatures. Heating cycles need to be employed,
1 3
as described below, to ensure complete formation of austenite preceding strain measurements during cooling.
A1033 − 10 (2015)
6. Ordering Information
6.1 When this practice is to be applied to an inquiry, contract, or order, the purchaser shall so state and should furnish the
following information:
6.1.1 The steel grades to be evaluated,
6.1.2 The test apparatus to be used,
6.1.3 The specimen configuration and dimensions to be used,
6.1.4 The thermal cycles to be used, and
6.1.5 The supplementary requirements desired.
7. Apparatus
7.1 This practice is applicable to several types of commercially available high-speed dilatometer apparatus, which have certain
common features. These include the capabilities for: heating and cooling a steel specimen in vacuum or other controlled
atmosphere; programmable thermal cycles; inert gas or liquid injection for rapid cooling; continuous measurement of specimen
dimension and temperature; and digital data storage and output. The apparatus differ in terms of method of specimen heating and
test specimen design.
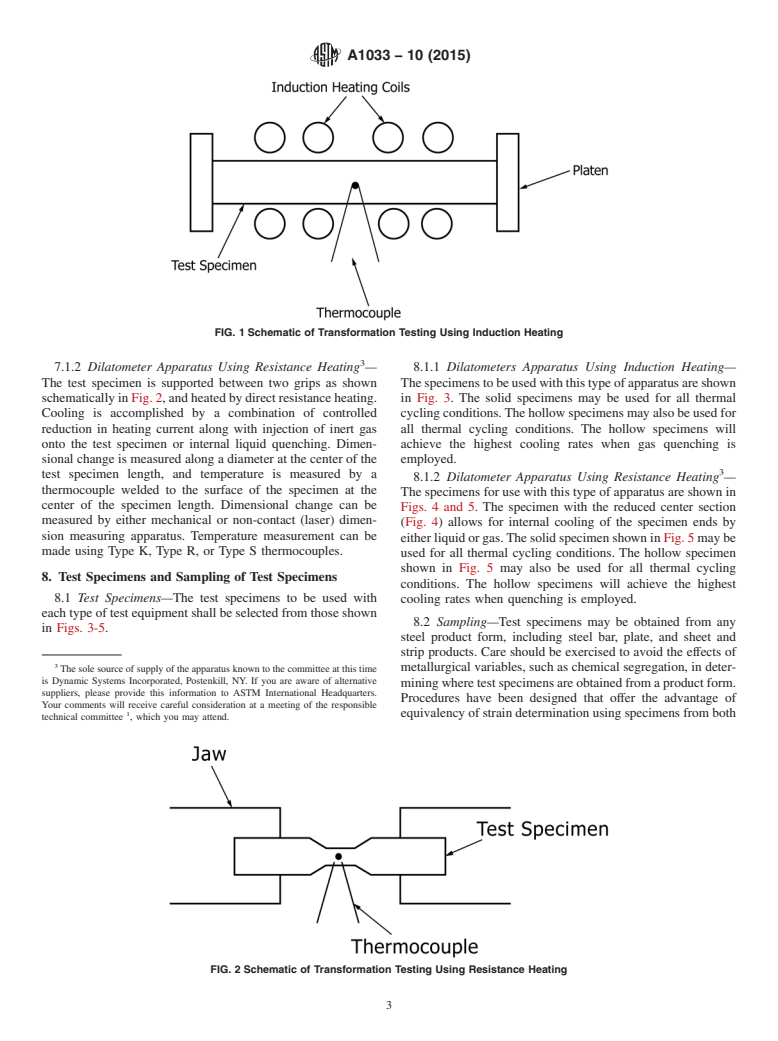
7.1.1 Dilatometer Apparatus Using Induction Heating—The test specimen is heated by suspending it inside an induction-
heating coil between two platens as shown schematically in Fig. 1. Cooling is accomplished by a combination of controlled
reduction in heating current along with injection of inert gas onto the test specimen. Dimensional change is measured by a
mechanical apparatus along the longitudinal axis of the test specimen, and temperature is measured by a thermocouple welded to
the surface of the specimen at the center of the specimen length. For this apparatus, only Type R or S thermocouples should be
used.
7.1.2 Dilatometer Apparatus Using Resistance Heating —The test specimen is supported between two grips as shown
schematically in Fig. 2, and heated by direct resistance heating. Cooling is accomplished by a combination of controlled reduction
in heating current along with injection of inert gas onto the test specimen or internal liquid quenching. Dimensional change is
measured along a diameter at the center of the test specimen length, and temperature is measured by a thermocouple welded to
the surface of the specimen at the center of the specimen length. Dimensional change can be measured by either mechanical or
non-contact (laser) dimension measuring apparatus. Temperature measurement can be made using Type K, Type R, or Type S
thermocouples.
8. Test Specimens and Sampling of Test Specimens
8.1 Test Specimens—The test specimens to be used with each type of test equipment shall be selected from those shown in Figs.
3-5.
8.1.1 Dilatometers Apparatus Using Induction Heating—The specimens to be used with this type of apparatus are shown in Fig.
3. The solid specimens may be used for all thermal cycling conditions. The hollow specimens may also be used for all thermal
cycling conditions. The hollow specimens will achieve the highest cooling rates when gas quenching is employed.
The sole source of supply of the apparatus known to the committee at this time is Dynamic Systems Incorporated, Postenkill, NY. If you are aware of alternative suppliers,
please provide this information to ASTM International Headquarters. Your comments will receive careful consideration at a meeting of the responsible technical committee
, which you may attend.
FIG. 1 Schematic of Transformation Testing Using Induction Heating
A1033 − 10 (2015)
FIG. 2 Schematic of Transformation Testing Using Resistance Heating
NOTE 1—All machining surface finishes being 0.8 μm RMS
FIG. 3 Test Specimens for Induction Heating Apparatus
8.1.2 Dilatometer Apparatus Using Resistance Heating —The specimens for use with this type of apparatus are shown in Figs.
4 and 5. The specimen with the reduced center section (Fig. 4) allows for internal cooling of the specimen ends by either liquid
or gas. The solid specimen shown in Fig. 5 may be used for all thermal cycling conditions. The hollow specimen shown in Fig.
5 may also be used for all thermal cycling conditions. The hollow specimens will achieve the highest cooling rates when quenching
is employed.
8.2 Sampling—Test specimens may be obtained from any steel product form, including steel bar, plate, and sheet and strip
products. Care should be exercised to avoid the effects of metallurgical variables, such as chemical segregation, in determining
where test specimens are obtained from a product form. Procedures have been designed that offer the advantage of equivalency
of strain determination using specimens from both types of apparatus described in 7.1.1 and 7.1.2. For equivalency of strain, the
orientation of the longitudinal axis of test specimens for induction heating apparatus should be at 90 degrees to the longitudinal
axis of specimens for resistance heating.
8.2.1 Example Sampling for Steel Bar Product Forms—Where material thickness permits, a selected test specimen should be
machined from the mid-radius position. Where material thickness is insufficient to permit machining a selected test specimen from
A1033 − 10 (2015)
NOTE 1—All machining surface finishes being 0.8 μm RMS
Test Specimen Dimension Guide Table
Reduced Section
Specimen Length, Specimen Half Length, Reduced Section Diameter, OD at Grip End, ID at Grip End, Grip End Drill Depth,
Length,
L1 ± 0.10 (mm) L2 ± 0.05 (mm) D3 ± 0.025 (mm) D1 ± 0.025 (mm) D2 ± 0.025 (mm) L4 ± 0.05 (mm)
L3 ± 0.025 (mm)
90 45 6 6 10 6.3 40
84 42 6 6 10 6.3 37
84 42 5 5 10 6.3 37
FIG. 4 Test Specimens with Reduced Center Section for Resistance Heating Apparatus
NOTE 1—All machining surface finishes being 0.8 μm RMS.
Test Specimen Dimension Guide Table
Reduced Section
Specimen Length, Speci
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.